01
Round Bar
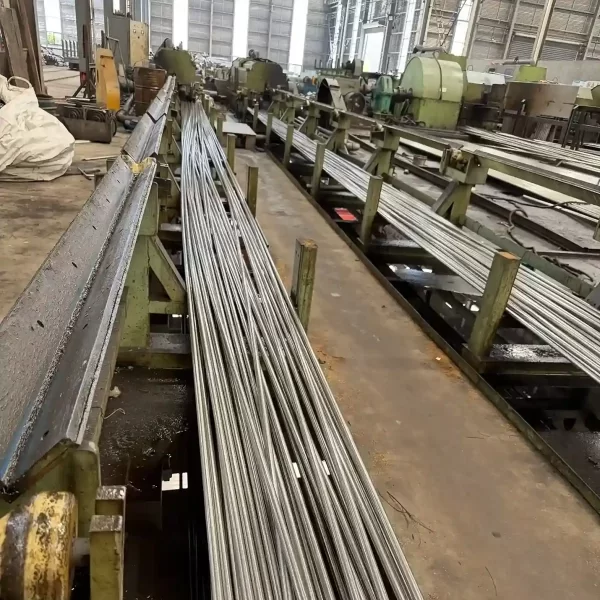
Hot-rolled rounds from 6 to 300 mm serve shafts, stems, and machined housings.
Request Availability →Copper-bearing nickel-iron-chromium bar for pump shafts, valve trim, and machined acid-plant parts.
The paperwork shows Nb+Ta against the carbon content, so the stabilisation claim can be verified.
Therefore, each heat carries a furnace chart and a quench record for the same lot.
Consequently, diameters past the bar range move to the forging route without a second supplier.
Alloy 20 bar arrives as a stabilised austenitic grade with copper in the matrix. Niobium at eight times the carbon content holds the grain boundaries clean through welding. Copper at 3 to 4% then carries the acid duty the part will see.
The bar route sits inside a wider family of forms, and each one names its own document. Meanwhile, round bar and rod follow the bar document, while heavier sections move to the forging route. Consequently, one heat can serve a pump shaft and its valve body at the same time.
However, the European trade also lists the grade as 20Cb-3, a Carpenter Technology trademark.
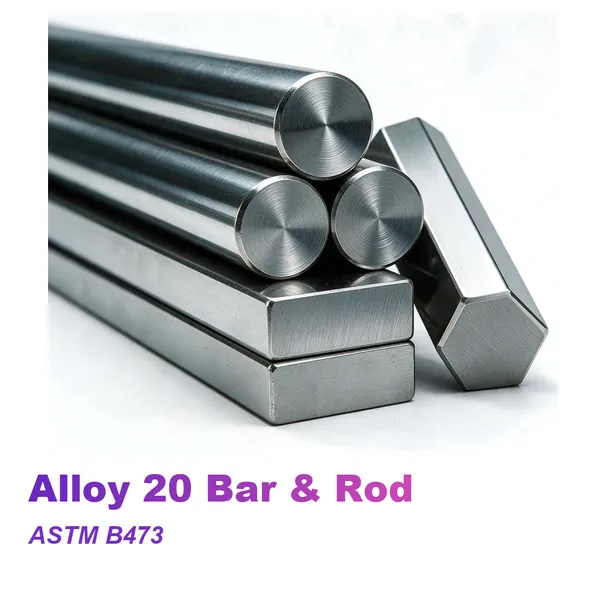
Alloy 20 bar carries the UNS N08020 grade, an austenitic nickel-iron-chromium alloy stabilised with niobium and alloyed with copper. Copper at 3 to 4% covers sulphuric and phosphoric acid duty, while niobium at eight times the carbon content keeps grain boundaries clean through welding. Nickel at 32 to 38% removes the chloride stress-corrosion cracking risk that limits 316L. Southerly Alloy supplies and exports UNS N08020 bar to ASTM B473, with heavier sections moving to ASTM B462.
Copper at 3 to 4% is the addition that opens sulphuric and phosphoric acid duty.
Nb+Ta at eight times the carbon content keeps grain boundaries clean through welding.
Nickel at 32 to 38% puts chloride stress-corrosion cracking out of reach.
Moreover, molybdenum at 2 to 3% and chromium at 19 to 21% widen the localised-attack window.
Also, the stabilised annealed condition machines cleanly, and no aging step follows.
Therefore, drawing or grinding lifts yield above the annealed floor where a shaft demands it.
In fact, each lot ships with the furnace chart and the quench record for its heat.
The grade appears in NACE MR0175 and ISO 15156-3, so oilfield projects can specify it.
Match the bar to the acid before anything else. Where dilute sulphuric or phosphoric acid dominates, this grade does the job at a fraction of nickel-molybdenum cost. Where chlorides run hot and concentrated, a higher-molybdenum grade takes over.
Copper at 3 to 4% keeps dilute sulphuric and phosphoric acid inside the working envelope.
Consequently, a welded body keeps its corrosion resistance without a furnace cycle.
Moreover, nickel at 32 to 38% takes stress-corrosion cracking out of the failure review.
In addition, we finish bar to the part drawing when the shop prefers a ready component.
Every lot follows one route, and each step leaves a record. Because the anneal and the quench decide the corrosion result, those two steps carry the tightest control.
Virgin nickel, chromium, copper, and molybdenum enter as weighed lots with the charge sheet signed off.
Argon-oxygen decarburisation drives carbon toward the 0.07% ceiling while residual sulphur and phosphorus stay low.
Specifically, niobium goes in at eight times the carbon content, which fixes the stabilisation ratio before the metal leaves the ladle.
Forging and rolling reduce the ingot between 760 and 1175 °C, and no pass finishes below 980 °C.
A furnace pass at 927 to 1010 °C dissolves the worked structure and equalises the composition.
Bars enter the tank straight from the furnace, because a slow cool would let carbides form at the grain boundary.
Drawing, peeling, or centerless grinding brings each bar to the ordered section.
Finally, the laboratory clears chemistry, tensile results, hardness, and dimensions before the lot ships.
Our manufacturing facility provides reliable production capacity for seamless pipes, tubes, fittings, plates and bars with strict quality management systems.
Melting, annealing, quenching, and finishing sit inside one boundary.
Sawing, turning, drawing, and grinding equipment covers every ordered section.
Custom heats and stock sizes run on the same campaign calendar.
A metallurgist reviews every acid duty enquiry before the offer goes out.
Documentation is the product here as much as the metal. Therefore, every lot leaves with a heat number that ties back to the melt, the anneal log, and the mechanical results.
The laboratory reads copper, niobium, and carbon, then compares each result with the ASTM window.
Moreover, mechanical values come from the delivered bar rather than a surrogate sample.
Diameter, straightness, and finish are measured before the lot is cleared for dispatch.
Consequently, every certificate carries a furnace chart reference and a quench record for the same heat.
Nine supply routes cover the shapes a machine shop asks for. In addition, each route names the document that governs it.
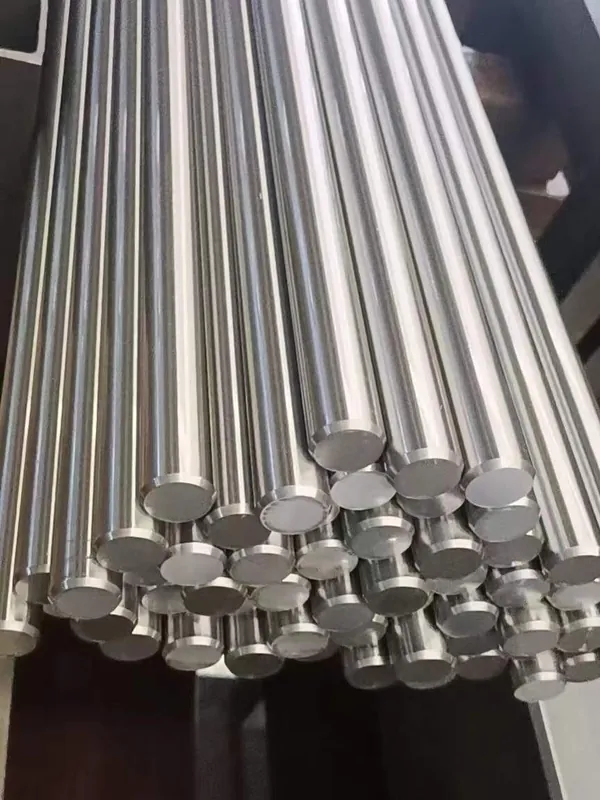
Hot-rolled rounds from 6 to 300 mm serve shafts, stems, and machined housings.
Request Availability →Similarly, drawn stock in coil or straight length suits fasteners and small turned parts.
Request Availability →A cold-drawn skin holds size over long automatic-lathe runs.
Request Availability →Drawing lifts yield above the annealed floor, and stress relief follows where the section needs it.
Request Availability →Across-flats stock suits bolting, nuts, and valve bodies.
Request Availability →Square sections carry frames, brackets, and welded fixtures.
Request Availability →Rectangular stock forms the base for racks and support grids.
Request Availability →Open-die forging covers valve bodies and heavy sections above the stocked range.
Request Availability →Centerless grinding holds the tolerance and finish that shaft seals demand.
Request Availability →Acid plant is where this grade has served longest. Meanwhile, the high nickel content makes chloride-bearing streams a second home.
Discuss Your Application →Shafts that turn in dilute sulphuric or phosphoric acid slurry.
Internal parts that see acid on one face and chloride on the other.
Plates drilled for tube bundles in acid coolers and interchangers.
Shell-side hardware in dilute and moderate acid duty.
Racks, hooks, and coil supports inside steel pickling baths.
Studs and bolting that must hold torque without cracking.
Components specified under NACE MR0175 and ISO 15156-3.
Shafts that survive alternating acid and caustic cleaning cycles.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The limits below come from ASTM B463, B473, and B729, which share one composition table for UNS N08020. Copper is the deliberate addition behind the acid performance, and the niobium range scales with the carbon content. The mill certificate governs final acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 32.0–38.0% |
| Chromium (Cr) | 19.0–21.0% |
| Copper (Cu) | 3.0–4.0% |
| Molybdenum (Mo) | 2.0–3.0% |
| Niobium + Tantalum (Nb+Ta) | 8 × C min., 1.00% max. |
| Manganese (Mn) | 2.00% max. |
| Silicon (Si) | 1.00% max. |
| Carbon (C) | 0.07% max. |
| Phosphorus (P) | 0.045% max. |
| Sulfur (S) | 0.035% max. |
| Iron (Fe) | Balance |
Bar and forged bar share one stabilised annealed condition, so the table below carries two rows rather than a full form list. Two footnotes matter for this route, and both are noted underneath.
| Product Form | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation | Hardness |
|---|---|---|---|---|---|
| Bar, rod, and wire, ASTM B473 | Stabilised annealed | ≥80 ksi (551 MPa) | ≥35 ksi (241 MPa) | 30% | 217 HB or 95 HRB max. |
| Forged bar and forging stock, ASTM B462 | Stabilised annealed | ≥80 ksi (551 MPa) | ≥35 ksi (241 MPa) | 30% | Not specified |
The bar document adds a 50% minimum reduction of area, and a strain-hardened condition carries its own row in the same standard. Wire takes a tensile window of 90 to 120 ksi (620 to 830 MPa) with no yield or elongation rule attached.
Indeed, cold work is the only strengthening route here, because the grade does not respond to aging. Therefore, a drawing that calls for higher yield needs a cold-drawn condition on the order.
The figures in this table are typical design values, and they are not acceptance limits. The alloy stays non-magnetic, and that suits instrument assemblies in acid circuits.
| Property | Value |
|---|---|
| Density | Approx. 8.08 g/cm³ |
| Melting range | Approx. 1385–1443 °C |
| Modulus of elasticity | Approx. 193 GPa |
| Shear modulus | Approx. 76 GPa |
| Thermal conductivity at 20 °C | Approx. 12.3 W/m·K |
| Electrical resistivity at 20 °C | Approx. 1.08 µΩ·m |
| Specific heat at 20 °C | Approx. 500 J/kg·K |
| Thermal expansion, 25–100 °C | Approx. 14.7 µm/m·K |
| Magnetic response | Essentially non-magnetic |
| Strengthening route | Cold work only |
Four ASTM documents cover the bar route and its two neighbours, and the ASME editions govern once a pressure code applies. In addition, no SAE aerospace specification reaches UNS N08020. The European and Chinese designations below serve cross-reference only.
| Standard | Product or Application |
|---|---|
| ASTM B473 / ASME SB473 | Bar, rod, and wire |
| ASTM B462 / ASME SB462 | Forgings and forged bar |
| ASTM B472 | Forging billets and bars for reforging |
| ASTM B463 / ASME SB463 | Plate, sheet, and strip cut from the same heat |
| NACE MR0175 / ISO 15156-3 | Sour service qualification for oil and gas |
| UNS N08020 | Unified Numbering System designation |
| W.Nr. 2.4660 / NiCr20CuMo | European designation |
| GB/T 15007 NS1403 | Chinese designation |
| SAE AMS | No aerospace specification covers this grade |
20Cb-3 and Carpenter 20 are trademarks of Carpenter Technology, and Incoloy is a trademark of Special Metals Corporation. We quote those names for reference only, and our deliveries follow the ASTM and ASME documents listed above.
The standard text from ASTM International settles any acceptance question.
Because the bar document sets its own scope, the ranges below follow that text rather than one house rule. For that reason, state the form and the ordered size on the enquiry.
| Product Form | Typical Supply Range |
|---|---|
| Hot-finished round bar | 6–300 mm diameter to ASTM B473 |
| Cold-finished round bar | 6–100 mm diameter, closer tolerance by agreement |
| Square and hexagon bar | 8–80 mm across flats |
| Flat bar | 3–150 mm thick, up to 300 mm wide |
| Wire and rod in coils | 1.5–12 mm diameter to ASTM B473 |
| Forged bar and forging stock | Sections above the agreed bar range to ASTM B462 and B472 |
Also, cut lengths run from 1 m up to 6 m as standard, and heavier sections move to the forging route. Therefore, give the ruling diameter on the enquiry so the correct document is quoted.
Finish follows the operation that comes next rather than a catalogue default. In short, we agree the surface with your order.
| Surface Condition | Typical Use |
|---|---|
| Stabilised annealed and pickled | Standard delivery for acid and chloride service |
| Hot-worked | As-rolled or as-forged surface for parts that will be machined |
| Cold drawn | Close diameter control with a brighter surface |
| Peeled | Uniform diameter with a machined skin for further turning |
| Centerless ground | Tight diameter and straightness for shafting |
| Polished | Reduced roughness for product-contact and visible parts |
| Bright annealed | Scale-free surface for instrument and clean circuits |
Get detailed information including specifications, standards, dimensions and material properties.
Eight steps turn an enquiry into a delivered lot. Therefore, send the drawing or the size list first, and the rest follows.
Give the acid, its concentration, the temperature, the diameter, and the quantity.
Tell us whether the part is welded, formed, or machined from solid.
We fix stabilised annealed, cold drawn, or forged against that route.
Price, lead time, and the certificate package reach you in one message.
Grade, size, inspection level, and delivery terms go on the record.
The mill takes the lot through melting, annealing, quenching, and release testing.
If the drawing asks for it, we finish the bar and inspect the finished part.
Finally, the desk tracks the shipment and sends the paperwork ahead of arrival.
Feedback from buyers and engineers who source nickel alloy materials from Southerly Alloy.
“Overall, the shafts held their diameter through two campaigns, and the acid attack stayed inside the allowance.”
“In short, one trial bar settled the finish question before we released the annual volume.”
“The certificate named copper and niobium, so incoming inspection cleared the lot without a second test.”
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B473 covers bar, rod, and wire. Forged bar and heavier sections follow B462, and forging billets follow B472.
Round bar runs from 6 to 300 mm diameter. Square and hexagon stock covers 8 to 80 mm across flats, and flat bar reaches 300 mm wide.
Niobium at eight times the carbon content ties carbon up as a stable carbide, so grain boundaries hold their chromium through welding.
Yes. Bars are quenched in water straight from the 927 to 1010 °C anneal, because a slow cool would let carbides form.
C-276 covers a wider acid range and higher chloride levels, and it costs considerably more. Alloy 20 wins on dilute sulphuric duty where the budget matters.
ER320LR for TIG and MIG, and E320LR for stick welding. In addition, both are low-residual grades that resist hot cracking.
One bar covers most stock sizes, and a short cut is enough for a trial.
We quote mainly on FOB terms, and EXW or CIF follow on request.
Stock diameters ship in 7-15 days, and made-to-order sections run about 25 days.
Yes. Every heat ships with an EN 10204 3.1 certificate, and we arrange 3.2 endorsement on request.
Send the diameter, the length, and the acid duty. We reply with price, lead time, and the certificate package in one message. Because bar above the agreed range moves to the forging document, state the heaviest section you need.
Additionally, a short trial run costs very little, so a single bar proves the grade before a plant-wide release.