01
Hot-Rolled Plate
Annealed and pickled flat product from 4.76 to 63.5 mm thick.
Request Availability →Flat-rolled product for welded linings and vessel internals in reducing acid service, stable enough to skip a second anneal.
The chromium window keeps a welded lining ductile where an earlier B-type sheet would embrittle.
Thickness and width together fix the classification, and we settle it before a price leaves the desk.
Bundles are interleaved and crated so the pickled surface arrives ready to fit.
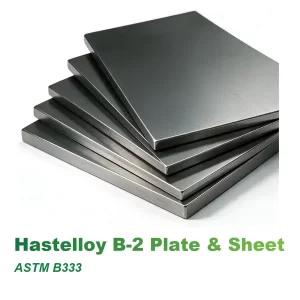
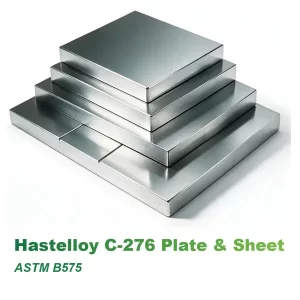
Hastelloy B-3 Plate and Sheet carries the UNS N10675 grade as flat-rolled product. Chromium between 1 and 3% slows the ordered phases, which matters when a lining is welded into place. Reducing acids leave the surface intact, while oxidants destroy it.
Flat product reaches fabricators as plate, sheet, and strip. Above all, welded linings and tray work are where this grade separates itself. The Hastelloy B-3 hub carries the alloy data, and the Hastelloy B-3 Bar and Rod and Hastelloy B-3 Pipe and Tube pages cover the other two routes.
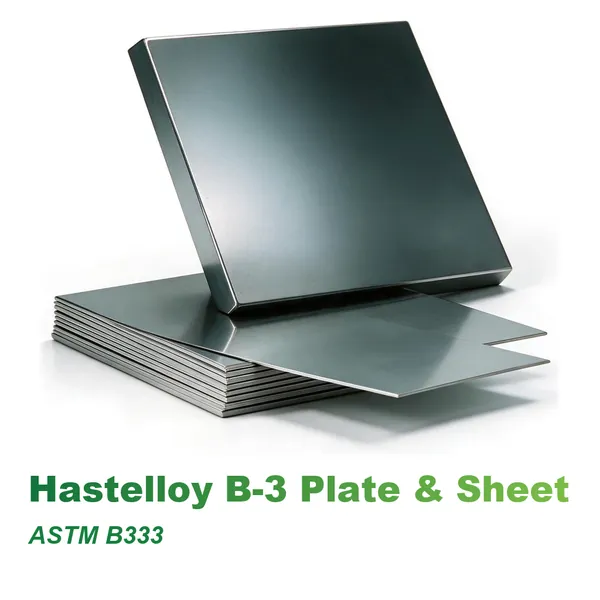
Hastelloy B-3 plate and sheet carries the UNS N10675 grade as flat-rolled product to ASTM B333. Chromium between 1 and 3 percent slows Ni4Mo ordering, which is what a welded lining needs once it cannot be re-annealed. The nickel-molybdenum chemistry resists hydrochloric and sulfuric acid while the stream reduces, and it refuses oxidants. Southerly Alloy works as a professional supplier and exporter of flat product from 4.76 to 63.5 mm plate down through light sheet and strip.
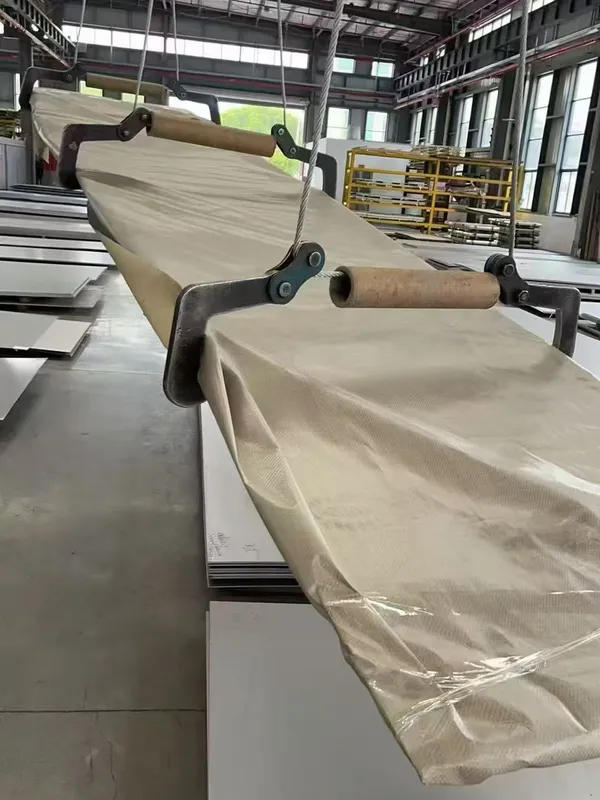
Chromium in the 1 to 3% range slows ordering, so a welded lining keeps far more ductility.
Moreover, carbon at 0.01% maximum lets most welded work enter service without a further anneal.
Hydrochloric and sulfuric acid cause little attack while the medium stays reducing.
In addition, formic and acetic media sit inside the working envelope.
A nickel-rich matrix resists cracking wherever chlorides collect under a lining.
Therefore, ASTM B333 covers plate from 4.76 to 63.5 mm thick.
Meanwhile, liners and formed parts draw on sheet and strip under 4.76 mm.
Consequently, flatness and edge condition go on the specification rather than staying open.
A welded lining rarely gets a second anneal once it sits in place. Therefore, the sheet has to carry its own ductility into service. That constraint is why most new linings specify this grade.
We ask how the sheet will be formed and welded, since that shapes the certificate set.
Each certificate names the melt, with the anneal record filed alongside the mechanical results.
Therefore, plate arrives cut to your length and width rather than in mill sizes.
Faces are interleaved and edges protected, then we quote FOB, CIF, or DAP.
A lining has to reach one annealed condition across its whole area, so thickness and temperature travel together through rolling. Therefore, the mill quenches each lot before shearing.
The slab is cleaned and inspected ahead of the first roll pass.
Rolling brings the slab down to plate thickness at temperature.
A furnace cycle restores ductility before the cold reduction begins.
Cold mills bring sheet and strip to final gauge with tight thickness control.
Holding near 1066 °C dissolves any ordered phase that earlier passes left behind.
The plate drops through the mid range fast, which keeps ordering from restarting.
An acid bath strips the scale so the face is ready to fit.
Flatness, gauge, and edge quality sign off before the bundle is packed.
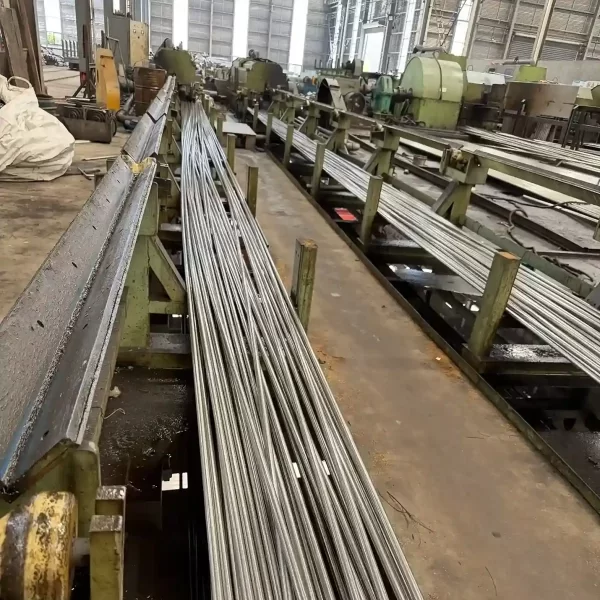
Flat-rolled work draws on the same melt shop and annealing furnaces as our tubular and bar lines. Consequently, one certificate set can cover a project that mixes all three forms.
The melt shop, rolling mills, and annealing furnaces sit on one site.
Hot mills, cold mills, and shears make up the equipment base.
Plate and sheet share a melting campaign with the bar and tube lines.
Lining design and weld procedure questions reach a specialist.
Release rests on evidence gathered before dispatch. The lab reads chemistry against the N10675 window, and gauge plus flatness records follow the plate.
Molybdenum, chromium, and carbon results land beside the B333 limits.
In addition, thickness, width, and flatness readings ride with the release papers.
Where the order names ASTM E112, the lab adds a grain size report.
Every figure on the certificate traces back to a single heat.
Flat product classifies by thickness and width, so the enquiry should carry both numbers. Therefore, we quote each band with its own tolerance.
Annealed and pickled flat product from 4.76 to 63.5 mm thick.
Request Availability →A smoother face and tighter gauge for vessel internals.
Request Availability →Under 4.76 mm thick, for ducting and loose liners.
Request Availability →Annealed sheet with an even face for formed components.
Request Availability →In addition, strip runs under 4.76 mm thick and under 600 mm wide, supplied coiled for press work.
Request Availability →Plate reaches you sheared or plasma cut to the ordered length and width.
Request Availability →A lining only works if the whole surface holds, so the medium and its temperature drive the choice. Meanwhile, welded vessels take most of the tonnage.
Discuss Your Application →Loose and clad liner sheet for hydrochloric acid vessels.
Trays and supports for chlorinated organics separation.
Absorber and duct plate for acidic flue-gas duty.
Shell and floor plate for reducing-acid storage.
Meanwhile, support and baffle plate for reducing-side exchangers.
Immersed sheet for hydrochloric and sulfuric pickling baths.
Product-contact sheet for acid-bearing streams.
Finally, duct runs where the joint cannot be re-annealed after fabrication.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The flat-product document carries the composition table for UNS N10675. Chromium in the 1 to 3% range is what keeps a welded face stable, and nickel plus molybdenum resists the acid. The mill certificate governs final acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 65.0% min. |
| Molybdenum (Mo) | 27.0–32.0% |
| Chromium (Cr) | 1.0–3.0% |
| Iron (Fe) | 1.0–3.0% |
| Tungsten (W) | 3.0% max. |
| Cobalt (Co) | 3.0% max. |
| Manganese (Mn) | 3.0% max. |
| Carbon (C) | 0.01% max. |
| Silicon (Si) | 0.10% max. |
| Phosphorus (P) | 0.030% max. |
| Sulfur (S) | 0.010% max. |
| Vanadium (V) | 0.20% max. |
| Aluminum (Al) | 0.50% max. |
| Titanium (Ti) | 0.20% max. |
| Copper (Cu) | 0.20% max. |
| Columbium (Nb) | 0.20% max. |
| Tantalum (Ta) | 0.20% max. |
| Zirconium (Zr) | 0.10% max. |
| Nickel plus Molybdenum | 94.0–98.0% |
Plate and light flat product share one set of minimums, and the table below splits them by thickness band. As a result, the ordered thickness tells you which row applies.
| Product Form | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation | Hardness |
|---|---|---|---|---|---|
| Plate, ASTM B333, 4.76–63.5 mm | Solution annealed and descaled | ≥110 ksi (760 MPa) | ≥51 ksi (350 MPa) | 40% | 100 HRB max. |
| Sheet and strip, ASTM B333, under 4.76 mm | Solution annealed and descaled | ≥110 ksi (760 MPa) | ≥51 ksi (350 MPa) | 40% | 100 HRB max. |
The grade is not age hardenable, so cold rolling is the only route to higher strength. Sheet ordered for deep drawing carries a grain size requirement beside the tensile figures.
Values below are typical room-temperature figures for design work rather than acceptance criteria. In addition, the alloy stays essentially non-magnetic in the annealed condition.
| Property | Value |
|---|---|
| Density | Approx. 9.22 g/cm³ |
| Melting range | Approx. 1370–1418 °C |
| Modulus of elasticity | Approx. 216 GPa |
| Modulus of rigidity | Approx. 83 GPa |
| Thermal conductivity at 20 °C | Approx. 11.2 W/m·K |
| Electrical resistivity at 20 °C | Approx. 1.37 µΩ·m |
| Thermal expansion, 25–100 °C | Approx. 10.6 µm/m·K |
| Magnetic behaviour | Essentially non-magnetic in the annealed condition |
ASTM B333 covers plate, sheet, and strip, and thickness plus width decides which name applies. Specifically, no SAE aerospace specification reaches UNS N10675. Meanwhile, the designations below identify the same melt.
| Standard | Product or Application |
|---|---|
| ASTM B333 / ASME SB333 | Plate, sheet, and strip in hot-rolled or cold-rolled condition |
| ASTM B906 | General requirements for flat-rolled nickel alloys |
| ASTM E112 | Grain size determination for sheet and strip |
| ASTM B335 / ASME SB335 | Rod in the same grade |
| ASTM B622 / ASME SB622 | Seamless pipe and tube |
| ASTM B619 / ASME SB619 | Welded pipe |
| ASTM B626 / ASME SB626 | Welded tube |
| ASTM B564 / ASME SB564 | Forgings |
| ASTM B366 / ASME SB366 | Factory-made wrought fittings |
| DIN 17750 | Flat product in wrought nickel alloys |
| ISO 6208 | Nickel alloy plate, sheet, and strip |
| UNS N10675 | Unified Numbering System designation |
| W.Nr. 2.4600 / NiMo29 | European designation for Alloy B-3 |
| GB/T 15007 NS3203 | Chinese designation |
| SAE AMS | No aerospace specification covers this grade |
The flat-product documents come from ASTM International, and their text settles any acceptance question.
Each band below follows the scope ASTM B333 sets, where thickness and width together fix the product name. For that reason, give both measurements on the enquiry.
| Product Form | Typical Supply Range |
|---|---|
| Plate | 4.76–63.5 mm thick, width above 250 mm |
| Sheet | Under 4.76 mm thick, width from 600 mm |
| Strip | Under 4.76 mm thick, width under 600 mm |
| Cut Plate | Sheared or plasma cut to ordered length and width |
| Coil | Strip supplied coiled for press and lining work |
A face finish decides how well a lining cleans and how long it holds. In short, we agree it with the order rather than assume a default.
| Surface Condition | Typical Use |
|---|---|
| Annealed and pickled | Standard delivery for hydrochloric and sulfuric acid service |
| Hot-rolled and descaled | Parts that will be machined or further formed |
| Cold-rolled, bright finish | Uniform face for vessel internals and visible panels |
| Bright annealed | Scale-free surface for clean and product-contact service |
| Polished | Reduced roughness for high-purity and decorative work |
Get detailed information including specifications, standards, dimensions and material properties.
A single coordinator follows your flat-product order from enquiry to delivery. We fix the classification, the flatness, and the edge before the mill starts.
Give the acid, its strength, the thickness, and the cut size.
We agree whether the order reads as plate, sheet, or strip.
Tell us how the sheet will be formed and welded in place.
Price, lead time, and the document set arrive together.
Grade, thickness, cut size, and delivery terms go on record first.
The mill rolls, anneals, quenches, and tests the plate against your order.
Export papers and certificates follow the plate under the agreed terms.
Finally, we keep you posted on the consignment until it lands.
Feedback from buyers and engineers who source nickel alloy materials from Southerly Alloy.
“The liner sheet welded into our HCl reactor without a post-weld anneal, which saved a furnace slot.”
“Gauge and flatness figures came with the certificate, so receipt inspection cleared the bundle quickly.”
“A trial sheet settled the pickled face before we released the tank lining order.”
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
B333 and ASME SB333, and they cover plate, sheet, and strip alike.
By thickness and width together, with plate starting at 4.76 mm and above 250 mm wide.
Usually yes, because the chromium window slows Ni4Mo ordering.
Yes, at every concentration up to boiling, provided no oxidant touches the face.
ERNiMo-7 wire to AWS A5.14 or ENiMo-7 covered electrodes to A5.11.
One plate covers the common stocked thicknesses.
FOB comes as standard, and EXW or CIF follows when you ask.
The figure follows weight, and the alloy share is frozen when you order.
Stocked thicknesses go out in 7-15 days, and custom rolling takes about 25 days.
Yes. A 3.1 certificate accompanies each lot, and we can arrange 3.2 endorsement.
Give us the medium, its strength, the thickness, and the cut size. Tell us how the sheet will be welded, because that decides the certificate set. Price, lead time, and the paperwork come back in one reply.
One trial sheet is enough to prove the pickled face, so a single piece can start the order.