01
Round Bar
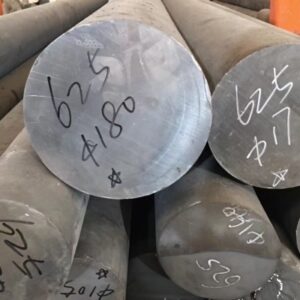
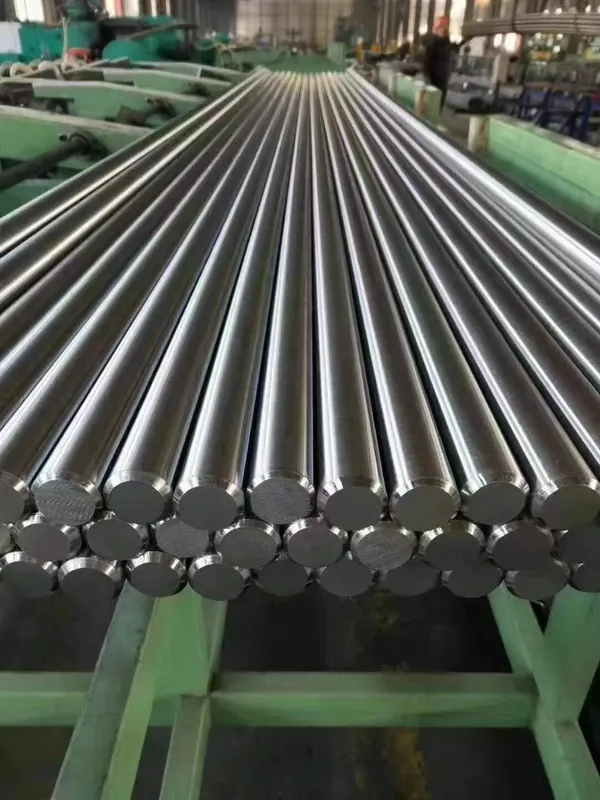
Solid rounds across the bar range feed pump shafts, valve trim, and machined reactor parts.
Request Availability →Low-iron nickel-chromium-molybdenum bar for shafts, valve trim, and machined parts that meet mixed acid duty.
The certificate shows iron and silicon against the ASTM limits, so a buyer can tell this grade from C-276 at a glance.
Consequently, the annealing and water-quench log travels with the heat number on every lot.
Therefore, diameters inside the bar document ship as bar, and anything heavier moves to the forging route.
Alloy 59 Bar and Rod carries the UNS N06059 grade, a nickel-chromium-molybdenum alloy built on a deliberately lean matrix. Iron stays at 1.5% maximum, silicon at 0.10% maximum. Therefore, the passive film reforms quickly after an upset, and the pitting resistance equivalent climbs toward 75.
The section and the delivery condition decide how the part performs, so the form pages carry the ordering detail. The bar range sits beside Alloy 59 Pipe and Tube and Alloy 59 Plate and Sheet in the same melt. The alloy background and the corrosion envelope sit on the Alloy 59 hub page.
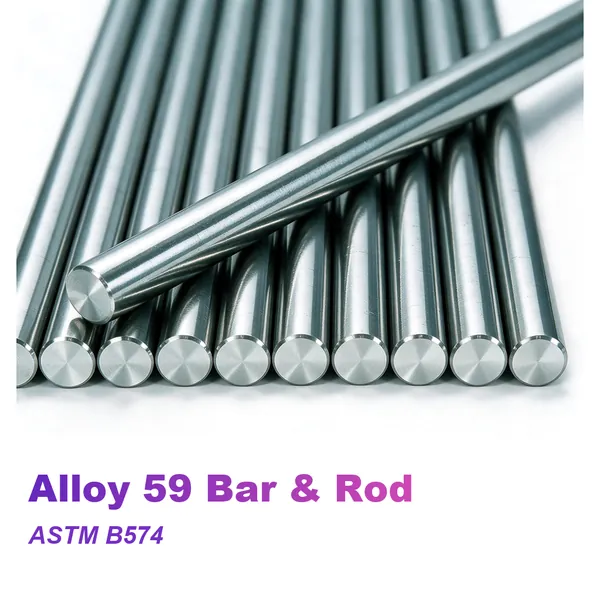
Alloy 59 bar and rod carries the UNS N06059 grade, a nickel-chromium-molybdenum alloy with iron held at 1.5% maximum and silicon at 0.10% maximum. That combination keeps the matrix close to a clean solid solution, which lifts pitting resistance and protects the weld zone. The grade serves acids that alternate between oxidising and reducing steps. Southerly Alloy works as a professional supplier and exporter of UNS N06059 bar to ASTM B574, with heavier sections moving to ASTM B564.
Iron at 1.5% maximum separates this grade from C-276, which allows up to 7%.
Moreover, silicon at 0.10% maximum slows the phases that drain weld-zone corrosion resistance.
Therefore, diameters from 6 to 300 mm ship to ASTM B574, with heavier sections quoted as forging stock.
Chromium at 22 to 24% and molybdenum at 15 to 16.5% cover oxidising and reducing media together.
Consequently, a pitting resistance equivalent near 75 handles chlorinated brine and seawater cooling duty.
In addition, drawing and peeling hold diameter and straightness for shafts, trim, and fittings.
The grade is not age hardenable, so cold work alone lifts yield above the annealed floor.
Every lot leaves the furnace straight into the quench tank, which locks the single-phase structure.
Start with the medium, because it decides whether this grade is the right one. Therefore, an acid stream that changes character between process steps carries the strongest case. However, price sits between C-276 and the leaner nickel alloys.
We report iron, silicon, and carbon against the ASTM window on every certificate.
Tensile results, quench log, and dimensional report all point back to the same melt.
We draw, peel, grind, or cut to length whenever the stocked section does not match.
Bar ends leave protected, and we quote FOB, CIF, or DAP against your port.
A lean matrix raises the sensitivity to slow cooling, so every lot gets a full anneal and a fast quench. Meanwhile, the finishing line holds the ordered diameter within the bar tolerance.
Virgin nickel, chromium, and molybdenum arrive as weighed lots with the tramp elements held low.
AOD refining drives carbon and silicon to the ceilings the grade allows.
Meanwhile, forging and rolling reduce the ingot between 950 and 1180 °C.
A furnace pass between 1100 and 1180 °C dissolves any phase that formed during reduction.
The bar drops straight into the tank while hot, because a delayed quench costs corrosion resistance.
Drawing, peeling, or grinding brings the bar to the ordered section.
An acid bath strips mill scale and leaves a surface ready for machining.
Finally, the lab clears chemistry, tensile properties, and dimensions before the lot ships.
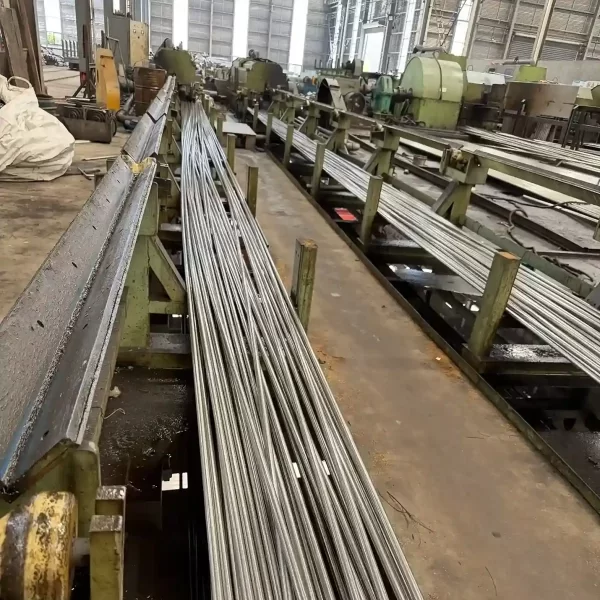
Our bar line shares one melt shop and one quench tank with the rest of the corrosion-resistant family. Consequently, a stocked diameter often ships without waiting for a furnace campaign.
Melt shop, quench tank, and finishing bays sit on one site.
Hot working, drawing, and grinding machines are installed and running.
Custom melts and stocked diameters share one production campaign.
A specialist reviews mixed acid and sour service duty before release.
Release rests on evidence rather than assumption. Chemistry runs against the N06059 window, and mechanical results follow the condition you ordered.
The lab reads iron, silicon, and molybdenum, then compares each figure with the ASTM limits.
Tensile, yield, and hardness values are taken from the lot you receive.
Diameter, straightness, and surface state are measured before the lot is packed.
Therefore, the heat number on the certificate points back to the annealing and cooling record.
How the part machines follows from the section you order, so state the form and the diameter. Therefore, each form carries its own condition and tolerance.
Solid rounds across the bar range feed pump shafts, valve trim, and machined reactor parts.
Request Availability →Drawn to fine tolerances in coil or straight lengths for fasteners.
Request Availability →Cold drawing leaves a smooth skin that holds size over long automatic-lathe runs.
Request Availability →Drawing raises yield beyond the annealed floor, with stress relief where straightness counts.
Request Availability →Across-flats stock fits bolting and valve components with several flats.
Request Availability →Square sections support frames and welded fixtures.
Request Availability →Rectangular stock to a given thickness and width forms the base strip for acid hardware.
Request Availability →Open-die work reaches valve bodies and diameters past the bar range.
Request Availability →Centerless grinding holds the tolerance and finish that shaft seals require.
Request Availability →Acid plant that runs more than one step carries the strongest case for this grade. Meanwhile, chloride-bearing streams benefit from the pitting margin.
Discuss Your Application →Tube plugs, baffle hardware, and trim machined from bar.
Agitator shafts and spray header fittings in wet scrubbers.
Stems, seats, and bodies qualified to NACE MR0175.
Shafting and sleeves for chlorinated seawater and brine circuits.
Machined parts for reactors and transfer lines in oxidising duty.
Quench nozzles and duct fittings exposed to acid condensate.
Agitator shafts and baffles that survive alternating acid and alkali cleaning.
Baffle bars and tie rods for exchangers running in mixed acid.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The limits below come from ASTM B574, which also governs bar, rod, and wire. Iron and silicon are the deliberate restraints behind the grade, and aluminium is the small deliberate addition. The mill certificate governs final acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | Balance |
| Chromium (Cr) | 22.0–24.0% |
| Molybdenum (Mo) | 15.0–16.5% |
| Iron (Fe) | 1.5% max. |
| Aluminum (Al) | 0.10–0.40% |
| Copper (Cu) | 0.50% max. |
| Manganese (Mn) | 0.50% max. |
| Cobalt (Co) | 0.30% max. |
| Silicon (Si) | 0.10% max. |
| Phosphorus (P) | 0.015% max. |
| Sulfur (S) | 0.010% max. |
| Carbon (C) | 0.010% max. |
The bar document sets one annealed condition across the range, so the table below holds a single row. A separate European data sheet applies a higher yield floor, and that regime is not the same as the ASTM one.
| Product Form | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation | Hardness |
|---|---|---|---|---|---|
| Bar and rod, ASTM B574 | Solution annealed | ≥100 ksi (690 MPa) | ≥45 ksi (310 MPa) | 45% | 100 HRB max. |
| Forged bar, ASTM B564 | Solution annealed | ≥100 ksi (690 MPa) | ≥45 ksi (310 MPa) | 45% | 100 HRB max. |
The hardness figures are informative only, and the standards bar their use as a basis for rejection. Because the grade resists aging, cold work is the only route above those floors. In addition, sections above roughly 100 mm may be agreed at reduced minimum values, so state the ruling diameter on the enquiry.
Values below are typical figures for design work rather than acceptance criteria. Moreover, the alloy stays essentially non-magnetic, which suits instrument and seal assemblies.
| Property | Value |
|---|---|
| Density | Approx. 8.6 g/cm³ |
| Melting range | Approx. 1310–1360 °C |
| Modulus of elasticity | Approx. 210 GPa |
| Thermal conductivity at 20 °C | Approx. 10.4 W/m·K |
| Electrical resistivity at 20 °C | Approx. 1.26 µΩ·m |
| Specific heat at 20 °C | Approx. 414 J/kg·K |
| Thermal expansion, 20–100 °C | Approx. 11.9 µm/m·K |
| Relative magnetic permeability at 20 °C | 1.001 max. |
| Strengthening route | Cold work only |
The bar range runs under one ASTM document, and the ASME edition takes over under pressure-code jurisdiction. Specifically, no SAE aerospace specification reaches UNS N06059. The European and Chinese designations below serve cross-reference only.
| Standard | Product or Application |
|---|---|
| ASTM B574 / ASME SB574 | Bar, rod, and wire in the solution-annealed condition |
| ASTM B564 / ASME SB564 | Forgings and forging stock above the bar range |
| ASTM B472 | Forging billets and bars for reforging |
| ASTM B575 / ASME SB575 | Plate, sheet, and strip in the same grade |
| ASTM B622 / ASME SB622 | Seamless pipe and tube in the same grade |
| ASTM B462 / ASME SB462 | Forged or rolled flanges and forged fittings |
| ASTM B366 / ASME SB366 | Factory-made wrought fittings |
| NACE MR0175 / ISO 15156-3 | Sour service qualification for oil and gas |
| DIN 17752 / 17744 | Bar, strip, and wire in the European system |
| VdTÜV 505 | German pressure-equipment approval |
| UNS N06059 | Unified Numbering System designation |
| W.Nr. 2.4605 / NiCr23Mo16Al | European designation |
| GB/T 15007 NS3311 | Chinese designation |
| SAE AMS | No aerospace specification covers this grade |
Nicrofer 5923 hMo is a trademark of VDM Metals, and Inconel and Incoloy are trademarks of Special Metals Corporation. We list these names for cross-reference only, and our bar ships to the ASTM and ASME documents above.
The product documents come from ASTM International, and their text settles any acceptance question.
Ranges below follow the scope the bar document defines, and heavier sections move to the forging route. For that reason, give the diameter and the quantity on the enquiry.
| Product Form | Typical Supply Range |
|---|---|
| Round bar | 6–300 mm diameter to ASTM B574 |
| Round rod | 6–25 mm diameter in coil or straight lengths |
| Bright bar | 6–100 mm diameter, cold drawn and ground |
| Hex bar | 8–60 mm across flats |
| Square bar | 8–100 mm square |
| Flat bar | 6–100 mm thick by 20–300 mm wide |
| Forged bar | 200–1000 mm diameter to ASTM B564 |
| Length | Random 3–6 m, or cut to the drawing |
Finish follows the next operation rather than a catalog default. In short, we agree it with the order so the surface suits the fabrication you have planned.
| Surface Condition | Typical Use |
|---|---|
| Solution annealed and pickled | Standard delivery for acid and chloride service |
| Hot-worked | As-rolled or as-forged surface for parts that will be machined |
| Cold drawn | Close diameter control with a brighter surface |
| Peeled | Uniform diameter with a machined skin for further turning |
| Centerless ground | Tight diameter and straightness for shafting |
| Polished | Reduced roughness for product-contact and visible parts |
| Bright annealed | Scale-free surface for instrument and clean circuits |
Get detailed information including specifications, standards, dimensions and material properties.
A single coordinator follows your order from the first enquiry to the last shipping paper. Nothing moves until the acid duty and the delivery condition agree.
Give the medium, its concentration, the diameter, and the quantity.
Tell us whether it sees welding, forming, or heavy machining.
We settle solution-annealed, cold-drawn, or forged against that route.
Price, lead time, and the certificate set reach you together.
Grade, size, inspection level, and delivery terms go on record first.
The mill runs the heat through melt, anneal, quench, and release testing.
Where the drawing calls for it, we finish the bar and inspect the finished section.
Finally, the desk follows the load and mails the paperwork before it docks.
Feedback from buyers and engineers who source nickel alloy materials from Southerly Alloy.
“The shafts held their diameter through a season of chlorinated brine duty, and the quench record satisfied our inspector.”
“A trial bar settled the pickled finish before we released the acid cooler order.”
“The certificate named iron and silicon, so our receiving check took an afternoon rather than a week.”
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B574. Above its range, heavier sections come as forged bar to ASTM B564.
We supply from 6 to 300 mm diameter, with the ruling section stated on the enquiry.
Iron holds at 1.5% maximum instead of 7%, and silicon at 0.10% maximum. That purity supports a higher pitting resistance equivalent.
Silicon sits low enough that slow cooling lets secondary phases form. Consequently, every lot leaves the furnace straight into the tank.
ERNiCrMo-13 wire to AWS A5.14, or ENiCrMo-13 covered electrodes to AWS A5.11.
Therefore, one piece covers most stock sizes.
We quote mainly on FOB terms, and EXW or CIF follow on request.
Nickel, chromium, and molybdenum drive the base, and the diameter, condition, and test scope set the rest.
Consequently, stock sizes ship in 7-15 days, and made-to-order material runs about 25 days.
Yes. Every heat ships with an EN 10204 3.1 certificate, and we arrange 3.2 endorsement on request.
Give the form, the diameter, and the acid duty on the enquiry. Our engineers answer with a quotation, a delivery date, and the certificate list. Because the quench practice changes what we can certify on a heavy section, tell us the ruling diameter.
A trial quantity costs little, so one bar proves the grade before a plant-wide order.