01
Inconel 601 Seamless Pipe
Hot-worked and cold-worked annealed pipe to ASTM B167 for furnace and reformer lines.
Request Availability →Seamless and welded UNS N06601 tube to B167, B163, and B516 for furnace, reformer, and heat-exchanger duty.
In addition, we quote B167 and B163 seamless product alongside B516 welded tube under one UNS N06601 enquiry.
Moreover, we hold aluminium at 1.0–1.7% inside a narrow band so the scale keeps forming through service.
In short, we compile chemistry, mechanical, and traceability records for reformer and incinerator review.
Inconel 601 Pipe and Tube covers UNS N06601, an alumina-forming grade for oxidizing furnace service. Because aluminium sits in the chemistry, the oxide scale stays attached where plain chromia scales flake away. We quote each length from B167, B163, or B516.
Grade-level data sits on the Inconel 601 hub, and we cover the two other forms on the Inconel 601 Bar and Rod and Inconel 601 Plate and Sheet pages.
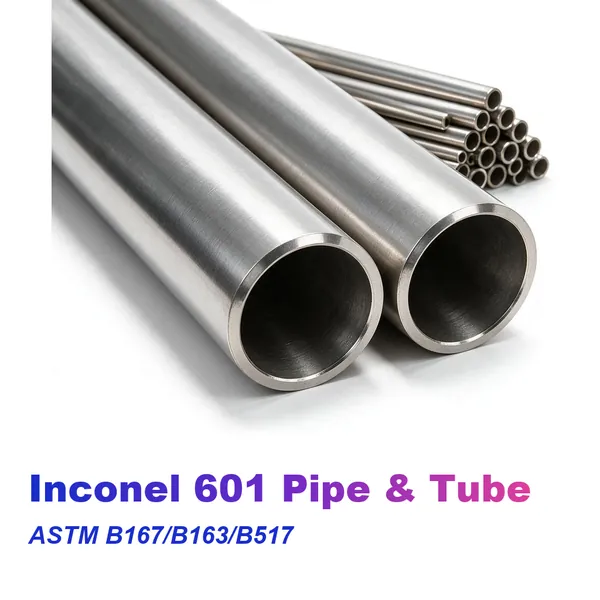
Inconel 601 pipe and tube covers seamless product to ASTM B167 and B163, plus welded tube to B516, quoted against schedule or drawing. Sizes run from precision exchanger tube to large-diameter furnace piping, delivered annealed or hot-finished. Aluminium at 1.0-1.7% forms the oxide scale that carries these lines past 1000 °C. EN 10204 3.1 certificates and heat-level traceability back furnace, reformer, and incinerator projects.
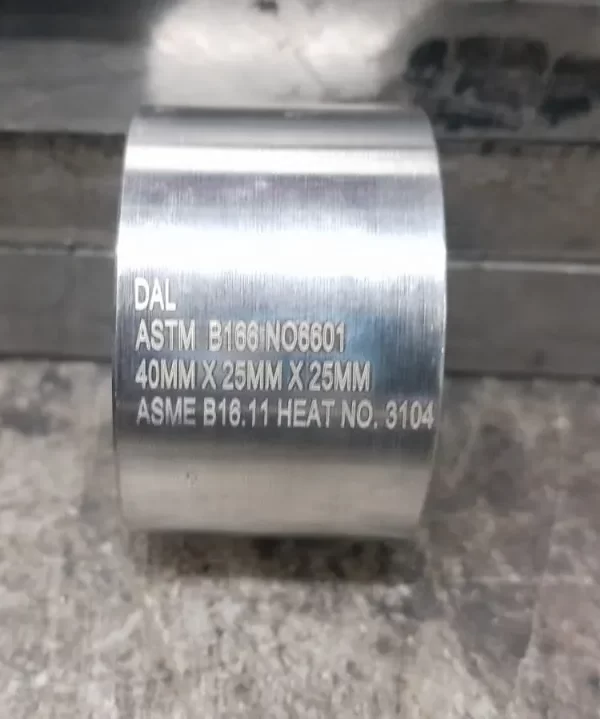
Above all, furnace tubing holds a protective scale in air well above the range where austenitic stainless grades scale away.
Tube survives carbon-rich and nitrogen-rich atmospheres that embrittle ordinary heat-exchanger materials.
B167 and B163 cover seamless product, while B516 governs the welded tube option.
In fact, repeated heat-up and cool-down leave the alumina scale intact, so we avoid spalling shutdowns.
In addition, chromium with aluminium tolerates oxidizing sulphur gases from oil- and gas-fired combustion.
Short-time tensile and creep strength stay useful well into the furnace temperature band.
Indeed, the 3.1 certificate carries the melting heat number for every length shipped.
For tubular work, Southerly Alloy keeps the commercial relationship while audited partner plants melt, pierce, and finish the tube. Also, your enquiry goes straight to the mill that runs that route. As a result, condition and documentation questions stay in one thread.
Moreover, we fix the manufacturing route against pressure, diameter, and budget before we issue the quotation.
In addition, we quote exchanger tube at 6 mm OD and furnace pipe at NPS 24 side by side.
We attach hydrostatic, eddy-current, PMI, and third-party inspection at order stage.
Therefore, we settle crating, Incoterm selection, and export documents before the tubes leave the plant.
Each UNS N06601 heat moves through melt, hot working, cold finishing, and annealing before release. Additionally, the route adjusts to the standard, condition, and acceptance level on the order.
We weigh nickel, chromium, and iron to the N06601 window, with aluminium added to a controlled target.
AOD or VOD refining holds carbon and sulphur in check, and ESR refines the ingot further where cleanliness demands it.
Billets are hot pierced or extruded into seamless shells, while welded tube starts from flat-rolled strip.
Cold pilgering or drawing brings exchanger and precision tube to the final outside diameter and wall.
We anneal the tube between 1100 and 1200 °C and cool it rapidly to set the oxide-forming structure.
We pickle, dimension-check, and test the product to the acceptance level named on the order.
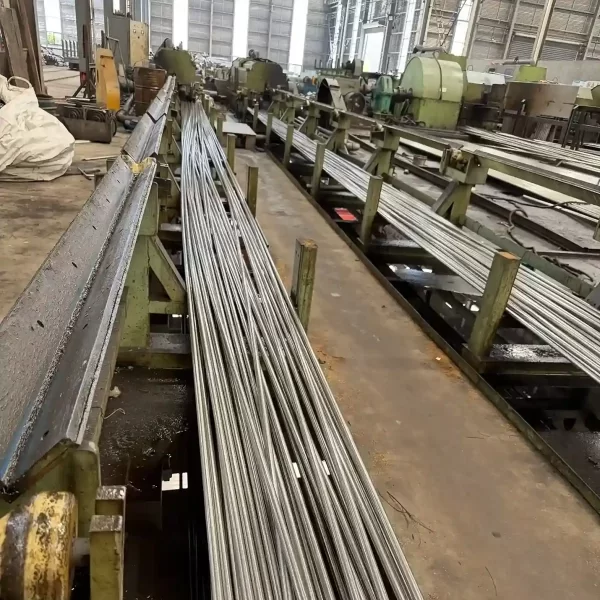
Seamless and welded UNS N06601 tube covers precision exchanger sizes through large furnace piping. We check each order against our rolling and annealing plan before production starts. Consequently, what we quote at enquiry is what leaves the plant.
Melting, tube rolling, and annealing halls sit on one production site.
Pilgering, drawing, welding, and finishing lines run under a single quality system.
Nickel alloy tubular output across stock and made-to-order sizes.
Metallurgists match the annealing condition to the furnace duty before release.
Before release, we clear every batch on chemistry, mechanics, dimensions, and surface. That verification runs inside the ISO 9001 system. Above all, a 3.1 certificate accompanies each shipment, and we add third-party inspection to the order when the buyer asks.
Specifically, a spectrometer analyses each heat, and we report the aluminium result with the chromium figure.
Tensile, yield, and elongation values come from the delivered condition and size band.
Moreover, we check OD, wall, straightness, and finish, with hydrostatic or eddy-current testing where specified.
Heat numbers on the certificate map each length back to its melting charge.
Overall, six tubular forms cover the UNS N06601 range, and each follows its own standard and finishing route.
Hot-worked and cold-worked annealed pipe to ASTM B167 for furnace and reformer lines.
Request Availability →Condenser and heat-exchanger tube to ASTM B163, with B829 general requirements applied.
Request Availability →Cold-worked and annealed welded tube to ASTM B516, formed from flat-rolled strip.
Request Availability →Large-diameter welded pipe quoted against B516 tube quality or the project specification.
Request Availability →Continuous coil and custom U-bends drawn from B163 base material for exchanger bundles.
Request Availability →Electropolished and bright annealed tube for clean chemical and high-purity duty.
Request Availability →Tubular duty here turns on furnace atmosphere and cycling rate rather than on liquid corrosion. Accordingly, the uses below pair oxidation or carburizing performance with the temperature each line carries.
Discuss Your Application →Furnace tubes and covers running hot in air between 900 and 1100 °C without shedding scale.
Retorts and support tubing exposed to carbon-rich atmospheres at temperature.
Petrochemical heater tubing carrying cyclic thermal stress in oxidizing gas.
Exchanger tubing above 800 °C where scale spalling, not pitting, limits service life.
Sheaths for sensors reading hot gas streams in boilers and incinerators.
Insulation cans, catalyst grids, and high-temperature process internals.
Components in waste incineration and thermal oxidizer gas paths.
Trays, baskets, and supports cycling through carburizing and nitriding campaigns.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The window below covers the B167, B163, and B516 tubular family for UNS N06601. Specifically, aluminium carries a narrow 1.0–1.7% range because it governs scale formation. However, the purchase specification in force decides acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 58.0–63.0% |
| Chromium (Cr) | 21.0–25.0% |
| Aluminium (Al) | 1.0–1.7% |
| Iron (Fe) | Balance |
| Carbon (C) | 0.10% max. |
| Manganese (Mn) | 1.00% max. |
| Silicon (Si) | 0.50% max. |
| Copper (Cu) | 1.00% max. |
| Sulphur (S) | 0.015% max. |
Overall, minimum room-temperature values below follow the governing standard, condition, and size band. Therefore, you must state the applicable ASTM condition for final acceptance.
| Product Form | Standard | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation |
|---|---|---|---|---|---|
| Seamless pipe and tube | ASTM B167 | Cold-worked or hot-worked annealed, all sizes | ≥550 MPa (80 ksi) | ≥205 MPa (30 ksi) | ≥30% |
| Heat-exchanger tube | ASTM B163 | Annealed | ≥552 MPa (80 ksi) | ≥207 MPa (30 ksi) | ≥30% |
| Welded tube | ASTM B516 | Cold-worked and annealed | ≥550 MPa (80 ksi) | ≥205 MPa (30 ksi) | ≥30% |
In addition, aerospace AMS 5715 deliveries carry condition-specific minimums and added process controls. State the condition at enquiry so we quote the correct standard.
In fact, the choice between Alloy 601 and Alloy 600 usually turns on furnace atmosphere rather than on liquid corrosion. Therefore, the table below sets the two chemistries side by side against the duty each one serves.
| Property / Feature | Inconel 601 (UNS N06601) | Inconel 600 (UNS N06600) |
|---|---|---|
| Governing Standard | ASTM B166 / B167 / B163 / B516 / B168 | ASTM B166 / B167 / B163 / B517 / B516 / B168 |
| Distinguishing Addition | Aluminium 1.0–1.7% | None — nickel-chromium-iron only |
| Chromium Level | 21.0–25.0% | 14.0–17.0% |
| Oxidation Ceiling | Cyclic service to about 1250 °C | Continuous service to about 1093 °C |
| Scale Behaviour | Alumina sub-scale resists spalling under cycling | Chromia scale sheds sooner in cyclic duty |
| Carburizing Resistance | Strong, because the alumina layer slows carbon pickup | Limited in carbon-rich atmospheres |
| Caustic and Chloride Duty | Moderate | Preferred grade for caustic and dry chlorine service |
| Typical Tubular Duty | Furnace tubes, reformer internals, incinerator parts | Caustic evaporators, dry chlorine lines, nuclear tubing |
| Property | Value |
|---|---|
| Alloy | Inconel 601 |
| UNS | N06601 |
| Werkstoff | 2.4851 |
| Density | Approx. 8.11 g/cm³ |
| Melting Range | Approx. 1360–1411 °C |
| Elastic Modulus | Approx. 206 GPa |
| Thermal Conductivity | Approx. 11.2 W/m·°C at 20 °C |
| Specific Heat | Approx. 450 J/kg·°C |
| Expansion Coefficient | Approx. 13.8 µm/m·°C (20–100 °C) |
| Alloy Type | Nickel-chromium-aluminium |
| Standard | Product / Application |
|---|---|
| ASTM B167 / ASME SB167 | Seamless pipe and tube, hot-worked and cold-worked |
| ASTM B163 / ASME SB163 | Seamless condenser and heat-exchanger tube |
| ASTM B516 / ASME SB516 | Welded tube, cold-worked and annealed |
| ASTM B829 | General requirements for seamless nickel alloy pipe and tube |
| ASTM B775 / B751 | General requirements for welded nickel alloy pipe and tube |
| SAE AMS 5715 | Bars, forgings, rings, and custom tube |
| DIN 17751 | Nickel alloy tube, W.Nr. 2.4851 |
| ISO 6207 | Nickel alloy seamless tube |
| EN 10095 | Heat-resisting steels and nickel alloys |
| UNS N06601 · W.Nr. 2.4851 · NiCr23Fe · JIS NCF 601 | Designations |
Document texts come from ASTM International. Where equipment falls under pressure-code jurisdiction, the ASME SB edition applies instead.
ASTM B517 covers welded nickel-chromium-iron pipe for UNS N06600 and related grades, but it does not list N06601. Welded Alloy 601 pipe is therefore quoted against B516 tube requirements or the project specification.
| Product Form | Typical Supply Range | Length |
|---|---|---|
| Seamless pipe | NPS 1/8 to NPS 24, SCH 10 to SCH 160 | Single random, double random, or custom |
| Seamless tube | OD 6–101.6 mm, wall 0.5–10 mm | Up to 12 m or custom cut lengths |
| Heat-exchanger tube | OD 6–76.2 mm, wall 0.7–6 mm | Up to 12 m or U-bend |
| Welded tube | OD 3.18–127 mm, wall 0.38–12.7 mm | Coil or fixed length |
| EP / BA tube | OD 6–50.8 mm, wall 0.5–3 mm | Up to 6–12 m, clean service |
| Coil / U-bend tube | OD 6–25.4 mm, wall 0.5–2 mm | Continuous coil or custom U-bend |
Overall, windows outside the listed range follow billet and strip availability. Therefore, give the OD, wall, length, condition, and end finish at enquiry so we can fix the route and price.
| Surface Condition | Typical Characteristics / Applications |
|---|---|
| Annealed & Pickled | Standard delivered condition for fabrication and installation |
| Bright Annealed | Smooth, scale-free bore and OD for instrumentation and clean service |
| Pickled Only | Acid-descaled surface for general industrial piping |
| Beveled End | Weld-preparation beveling to the agreed standard for butt welds |
Get detailed information including specifications, standards, dimensions and material properties.
A tubular order usually ships two to four weeks after release, though heavy-wall welded product takes longer. Before we fix the price, the steps below line up standard, condition, and acceptance with your duty.
Give the OD, wall, length, quantity, and ordered condition, plus the gas and peak temperature involved.
Seamless work runs to B167 or B163, while welded tube runs to B516.
Annealed tube favours bending and welding, while we choose hot-finished product for strength.
Price reflects the route, test scope, documentation, and Incoterm you picked.
The plant manufactures and tests to the acceptance level agreed when we placed the order.
Finally, tubes leave with 3.1 certificates, packing list, and the full export document set.
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
Buyers order seamless pipe and tube to ASTM B167, while condenser and heat-exchanger tube follow B163. Under code jurisdiction the ASME SB editions apply.
Published data documents cyclic oxidation service in air to roughly 1250 °C (2282 °F). However, you should confirm the design temperature against atmosphere, load, and pressure for each line.
ERNiCr-3 wire to AWS A5.14 pairs with ENiCrFe-3 electrodes to A5.11 for most joints. In addition, shop or field welding rarely requires preheat.
Yes. Coils and U-bends come from B163 base stock, formed against your own bending drawings.
Welded tube to B516 runs from OD 3.18 mm to 127 mm, with walls from 0.38 mm to 12.7 mm. We quote larger or heavier sections on request.
Overall, one piece covers many stock sizes, so trial lengths and repair pieces carry no premium hurdle.
FOB is the default Incoterm, while EXW, CIF, and DAP quotes follow confirmed destinations.
Pricing follows the ordered size, wall, and condition, and we normally calculate it by weight in kilograms. We confirm the applicable Incoterm on the offer.
Stock sizes ship in 7-15 days, while we quote made-to-order and heavy-wall tubular product against the production schedule.
Yes. Each delivery carries an EN 10204 3.1 certificate, and we can arrange third-party 3.2 endorsement on request.
Give the OD, wall, length, standard, and quantity at enquiry, and the reply returns price, Incoterm, lead time, and document list. In addition, route and testing questions can travel with the same message.