01
Hastelloy C-276 Bar and Rod
Likewise, round, hex, square, and forged bar to ASTM B574 come in solution-annealed or hot-finished condition.
View Hastelloy C-276 Bar and Rod →Nickel-molybdenum-chromium grade data for UNS N10276 / W.Nr. 2.4819 — composition, standards, and three supply forms.
Molybdenum and tungsten carry reducing acids while chromium handles oxidizing streams, so one grade covers both duties.
Bar, tubular, and flat-product enquiries run through the same commercial desk from first question to shipment.
EN 10204 3.1 documents link each consignment back to its melting heat for incoming checks.
Hastelloy C-276 is a nickel-molybdenum-chromium alloy that holds tungsten in solid solution. Its ultra-low carbon and silicon limits starve the grain-boundary precipitates that embrittle welded joints. Molybdenum and tungsten defeat reducing acids, while chromium covers oxidizing media.
The tables below arrange the grade data for specification review — composition, standards, and mechanical minimums by form. Detailed sizes and supply conditions sit on the Hastelloy C-276 Bar and Rod, Hastelloy C-276 Pipe and Tube, and Hastelloy C-276 Plate and Sheet pages.
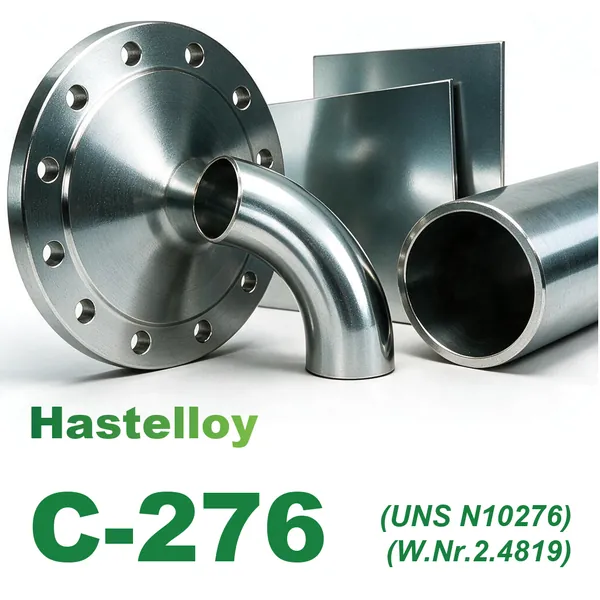
Hastelloy C-276 is a nickel-molybdenum-chromium-tungsten grade covering bar and rod, pipe and tube, and plate and sheet under the B574, B622, B619, B626, and B575 family. Molybdenum at 15.0-17.0% resists reducing acids, chromium at 14.5-16.5% covers oxidizing media, and tungsten at 3.0-4.5% reinforces the passive film. Because carbon stays at 0.010% max, welded joints keep their corrosion resistance in the as-welded state. This page collects composition, standards, and mechanical minimums for UNS N10276.

Overall, chromium, molybdenum, and tungsten tolerate nitric, sulphuric, hydrochloric, and blended acid streams.
In addition, molybdenum at 15.0–17.0% suppresses pitting and crevice attack in seawater, brine, and chloride process liquor.
Moreover, the nickel-rich matrix shrugs off chloride-induced cracking that splits austenitic stainless grades.
Carbon at 0.010% max and silicon at 0.08% max leave no carbides to precipitate, so as-welded joints keep their resistance.
Therefore, a water-quenched anneal between 1120 and 1160 °C dissolves precipitates before the material leaves the plant.
Indeed, hypochlorite, chlorine dioxide, and moist chlorine gas attack few materials this slowly.
Sour duty runs to NACE MR0175 / ISO 15156, backed by per-heat hardness records.
Consequently, the alloy stays practically non-magnetic at ambient temperature, which suits instrument and sensor assemblies.
For this grade, Southerly Alloy handles the commercial side while audited partner plants melt, roll, and finish the material. Your enquiry routes to the mill that owns that production step. Consequently, specification and shipment questions stay in one thread.
We fix carbon, silicon, and tungsten targets before the melt, so the certificate matches the order.
Medium, concentration, and temperature shape the grade guidance we return with the quotation.
In addition, EN 10204 3.1 certificates, PMI, and third-party witness attach to the order on request.
Packing method, Incoterm, and destination paperwork settle alongside the production plan you approve.
Three supply routes carry this grade, and each one has a page covering its own sizes, standards, and conditions.
Likewise, round, hex, square, and forged bar to ASTM B574 come in solution-annealed or hot-finished condition.
View Hastelloy C-276 Bar and Rod →Seamless product to B622, with welded pipe to B619 and welded tube to B626.
View Hastelloy C-276 Pipe and Tube →Hot-rolled plate and cold-rolled sheet to ASTM B575 in the solution-annealed condition.
View Hastelloy C-276 Plate and Sheet →This grade enters service where one stream mixes oxidizing and reducing attack, so the medium and its temperature decide material life. Accordingly, the uses below pair each environment with the form that carries it.
Discuss Your Application →Absorber vessels, spray headers, and ducting for chloride-bearing slurry.
Hypochlorite, chlorine dioxide, and moist chlorine streams that destroy stainless steel.
Reactors, evaporators, and piping across wide concentration ranges.
For example, digesters, agitators, and evaporator bodies for wet-process acid trains.
Digesters, bleach towers, and blow-line hardware in chlorine dioxide service.
Wellhead components and process piping for H2S-bearing duty.
Exchangers, pumps, and valves for chloride-rich cooling circuits.
Reactor vessels and transfer piping where metal pickup must stay minimal.
Ducting and scrubber parts that handle acidic combustion products.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The window below follows the ASTM product family for UNS N10276. Molybdenum and tungsten set reducing-acid and localised-corrosion resistance, chromium covers oxidizing media, and carbon stays ultra-low to protect weld zones. However, the governing purchase specification decides acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 57.0% min. (balance) |
| Molybdenum (Mo) | 15.0–17.0% |
| Chromium (Cr) | 14.5–16.5% |
| Tungsten (W) | 3.0–4.5% |
| Iron (Fe) | 4.0–7.0% |
| Cobalt (Co) | 2.50% max. |
| Manganese (Mn) | 1.00% max. |
| Vanadium (V) | 0.35% max. |
| Silicon (Si) | 0.08% max. |
| Carbon (C) | 0.010% max. |
| Phosphorus (P) | 0.040% max. |
| Sulphur (S) | 0.030% max. |
Minimum room-temperature values below come from the governing standard, and labs test every form of this grade in the solution-annealed condition. Because the ordered form fixes the applicable document, state the standard at enquiry.
| Product Form | Standard | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation |
|---|---|---|---|---|---|
| Bar and rod | ASTM B574 | Solution annealed | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Seamless pipe and tube | ASTM B622 | Solution annealed | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Welded pipe | ASTM B619 | Solution annealed after welding | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Welded tube | ASTM B626 | Solution annealed after welding | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Plate, sheet, and strip | ASTM B575 | Solution annealed | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Forgings and flanges | ASTM B564 | Solution annealed | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
Hardness on annealed product normally falls at or below 100 HRB. Aerospace deliveries run to AMS 5750 for bar, forgings, and rings, and to AMS 5530 for plate, sheet, and strip. State the required condition at enquiry, and we apply the right document.
| Property | Value |
|---|---|
| Alloy | Hastelloy C-276 |
| UNS | N10276 |
| Werkstoff | 2.4819 |
| Density | Approx. 8.89 g/cm³ |
| Melting Range | Approx. 1325–1370 °C |
| Elastic Modulus | Approx. 205 GPa |
| Thermal Conductivity | Approx. 10.2 W/m·°C at 20 °C |
| Specific Heat | Approx. 427 J/kg·°C |
| Expansion Coefficient | Approx. 11.2 µm/m·°C (20–100 °C) |
| Electrical Resistivity | Approx. 1.30 µΩ·m at 20 °C |
| Alloy Type | Nickel-molybdenum-chromium with tungsten |
| Strengthening | Solid solution and cold work |
| Magnetic Behaviour | Practically non-magnetic at ambient temperature |
| Standard | Product / Application |
|---|---|
| ASTM B574 | Rod and bar in the solution-annealed condition |
| ASTM B622 | Seamless pipe and tube, cold-finished or hot-finished |
| ASTM B619 | Welded pipe, solution annealed after welding |
| ASTM B626 | Welded tube for heat exchangers, condensers, and evaporators |
| ASTM B575 | Plate, sheet, and strip |
| ASTM B564 | Forgings and flanges |
| ASTM B366 | Wrought fittings in the same grade |
| ASTM B829 / B775 / B751 | General requirements for seamless and welded product |
| ASTM B906 | General requirements for nickel alloy flat-rolled product |
| ASME SB574 / SB622 / SB619 / SB626 / SB575 | Counterparts for pressure-code jurisdiction |
| SAE AMS 5750 | Bars, forgings, and flash-welded rings |
| SAE AMS 5530 | Plate, sheet, and strip |
| NACE MR0175 / ISO 15156 | Sour service in oil and gas production |
| DIN 17750 / 17751 / 17752 | Wrought nickel alloy flat product, tube, and bar |
| ISO 6207 / 6208 / 9723 | Nickel alloy tube, flat product, and bar |
| UNS N10276 · W.Nr. 2.4819 · NiMo16Cr15W · NS334 | Designations |
ASTM International issues these documents. Once equipment comes under pressure-code jurisdiction, the ASME SB edition governs instead. Sour-service projects, meanwhile, reference NACE MR0175 / ISO 15156 alongside the product standard.
| Product Form | Typical Supply Range |
|---|---|
| Bar and rod | 3–340 mm dia. by section and condition |
| Seamless pipe | NPS 1/8 to NPS 24, SCH 10 to SCH 160 and custom wall |
| Seamless tube | OD 6–114.3 mm, wall 0.5–10 mm |
| Welded pipe and tube | OD 3.18–127 mm, wall 0.38–12.7 mm |
| Plate and sheet | 0.5–100 mm thick, cut to length and width |
| Strip and coil | 0.5–6.35 mm thick, slit to width |
Size windows move with standard and condition, and heavier sections depend on slab or billet supply. Therefore, quote the diameter, wall or thickness, and length at enquiry so the route is accurate.
| Surface Condition | Typical Characteristics / Applications |
|---|---|
| Solution Annealed & Pickled | Standard delivery for acid, chloride, and seawater service |
| Bright Annealed | Scale-free surface for clean and visible applications |
| Pickled Only | Acid-descaled finish for general industrial work |
| Hot-Worked | As-rolled or as-forged surface for parts machined to size |
| Cold Drawn | Close diameter control with a bright finish |
Get detailed information including specifications, standards, dimensions and material properties.
Seamless tubular product runs to B622, welded pipe to B619, welded tube to B626, flat product to B575, and bar and rod to B574. Under pressure-code jurisdiction the ASME SB editions apply instead.
Carbon stays at 0.010% max and silicon at 0.08% max, so grain-boundary carbides cannot form in the weld heat-affected zone. Consequently, most joints enter service without post-weld heat treatment.
Supplier data documents continuous air service to roughly 540 °C, while intermittent duty reaches higher. However, the medium and its concentration usually set the real limit, so confirm the duty at enquiry.
ERNiCrMo-4 wire to AWS A5.14 pairs with ENiCrMo-4 electrodes to A5.11 for most joints. In addition, shop and field welding rarely needs preheat.
Molybdenum at 15.0–17.0% with tungsten at 3.0–4.5% suppresses pitting and crevice attack in seawater and brine. As a result, it suits once-through cooling circuits and offshore hardware.
A single piece covers most stock sizes, so trial quantities and repair lots carry no premium hurdle.
FOB serves as the default Incoterm, while EXW, CIF, and DAP quotes follow confirmed destinations.
Quotations follow the ordered form, size, and condition, and we normally calculate them by weight (kg). We state the applicable Incoterm on every offer.
Stock sizes run 7-15 days, and made-to-order sections are quoted against the confirmed production schedule.
Yes. Every delivery ships with an EN 10204 3.1 certificate, and 3.2 endorsement through a third party is available on request.
Send the grade, form, standard, size, and quantity, and we reply with price, Incoterm, lead time, and document list. Medium and temperature questions can ride along in the same message.