01
Seamless Tube
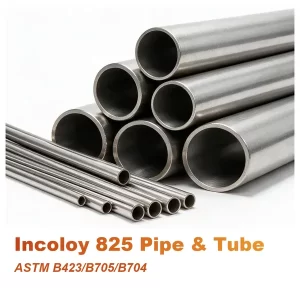
Cold drawn and annealed to ASTM B729, from 6 to 219 mm outside diameter.
Request Availability →Niobium-stabilised nickel-iron-chromium tube with copper, for acid coolers, exchanger bundles, and transfer lines.
Seamless, welded pipe, and welded tube each carry their own ASTM number on the offer.
Therefore, the certificate for every bundle points back to the furnace record and the quench log.
Consequently, niobium stabilisation lets a fabricated exchanger go to service as welded.
Alloy 20 tube handles the acid that moves between vessels rather than the metal that sits in it. Seamless product covers the pressure duty, and welded product covers the larger diameters. Copper at 3 to 4% keeps dilute sulphuric and phosphoric acid in range.
Tubular product sits beside the bar and the flat product in one family, and each route names its own document. Meanwhile, seamless tube follows the tube document, and welded pipe and welded tube follow their own. As a result, a heat can supply exchanger tubes and the shell pipe around them.
However, the trade also markets the grade as 20Cb-3, and Carpenter Technology owns that name.
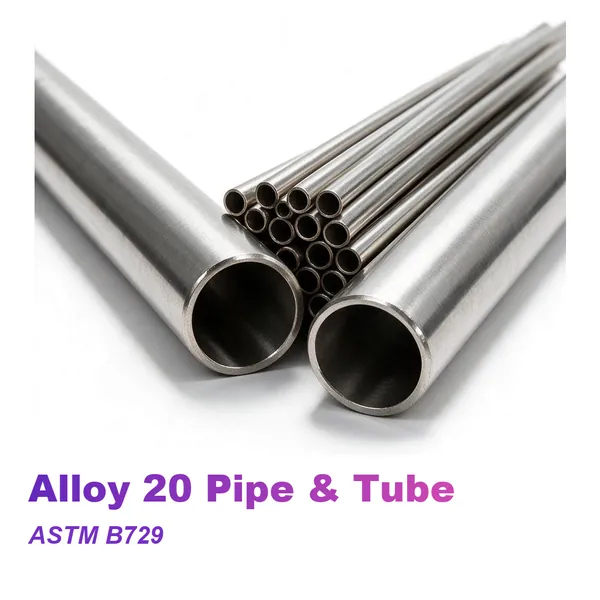
Alloy 20 pipe and tube carries the UNS N08020 grade, an austenitic nickel-iron-chromium alloy stabilised with niobium and alloyed with copper. Copper at 3 to 4% keeps dilute sulphuric and phosphoric acid inside the working envelope, and nickel at 32 to 38% removes chloride stress-corrosion cracking from the failure list. Niobium at eight times the carbon content means welded bundles need no post-weld anneal. Southerly Alloy supplies and exports UNS N08020 seamless tube to ASTM B729, welded pipe to B464, and welded tube to B468.
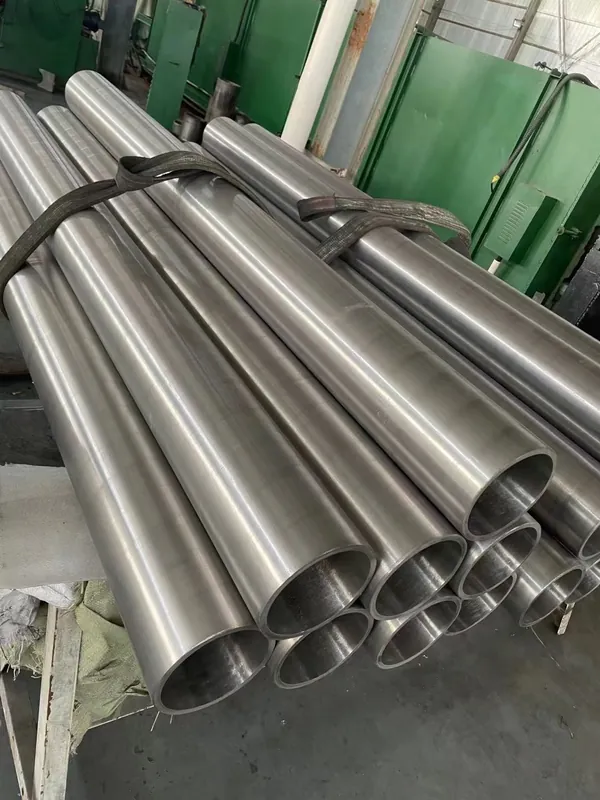
Copper at 3 to 4% keeps sulphuric and phosphoric acid inside the working envelope.
In fact, one heat supplies seamless tube, welded pipe, and welded tube.
Nickel at 32 to 38% removes chloride stress-corrosion cracking from the failure list.
Moreover, niobium stabilisation means a fabricated bundle needs no post-weld anneal.
Cold drawing and anneal give a wall that holds its thickness around the circumference.
Therefore, the ASME editions take over once a pressure vessel or piping code applies.
Specifically, the grade appears in NACE MR0175 and ISO 15156-3 for oilfield duty.
Low-residual filler metals match the base metal without a mismatch in the weld zone.
Start with the duty and the diameter together. Where dilute acid runs at moderate temperature, seamless Alloy 20 tube outlasts 316L and costs far less than a nickel-molybdenum grade. Where the chloride level climbs, a higher-molybdenum alloy takes over.
Indeed, copper at 3 to 4% carries dilute sulphuric and phosphoric duty that defeats 316L.
Consequently, a welded exchanger bundle goes to service without a second anneal.
Nickel at 32 to 38% keeps stress-corrosion cracking out of the design review.
In addition, we supply U-bend and coiled tube cut to the bundle drawing.
Tubular product runs through the same mill as the bar, on its own line. The anneal and the quench decide the corrosion result here too, so both steps stay under chart control.
A weighed billet from an approved heat becomes the starting stock for every seamless tube.
The mill pierces the billet, then rolls it to the ordered outside diameter and wall.
Drawing passes bring the tube to final size and tighten the wall tolerance.
We clean each length before the furnace so no residue carries into the anneal.
The charge holds at 982 to 1010 °C until the whole load reaches temperature.
Consequently, the tube enters the quench straight from the furnace to hold the carbon in solution.
The line straightens, squares, and cuts each length to the ordered figure.
Finally, the pressure test, the flattening test, and the dimensional check release the lot.
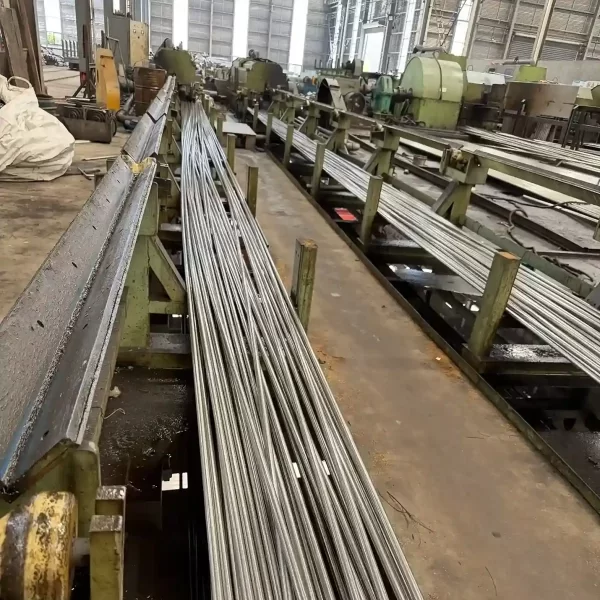
Our manufacturing facility provides reliable production capacity for seamless pipes, tubes, fittings, plates and bars with strict quality management systems.
Piercing, drawing, annealing, and testing share one site.
Draw benches, pilger mills, and straighteners cover the seamless range.
Seamless and welded product run on one campaign calendar.
A metallurgist reviews every acid and sour duty enquiry before the offer.
Every tube leaves with a document set that matches the standard behind it. Therefore, the heat number ties the certificate back to the melt, the anneal chart, and the test results.
The laboratory reads copper, niobium, and carbon, then checks each result against the limits.
Tensile and yield values come from the delivered product, not from a surrogate sample.
Hydrostatic proof and flattening checks release each lot for the welded routes.
Where the order calls for it, eddy current testing runs alongside the gauge check.
Five supply routes cover the tubular shapes a project asks for. In addition, every route carries its own acceptance document.
Cold drawn and annealed to ASTM B729, from 6 to 219 mm outside diameter.
Request Availability →Heavier wall stock for pressure lines under code jurisdiction.
Request Availability →Automatic welding without filler to ASTM B464, NPS 1/8 to 6 in Schedule 5S, 10S, and 40S.
Request Availability →Longitudinal weld to ASTM B468, from 3.2 to 88.9 mm outside diameter.
Request Availability →Bent lengths and coils cut to the bundle or coil drawing.
Request Availability →Acid plant and heat transfer are where this grade has served longest. Meanwhile, the high nickel content makes chlorinated cooling water a second home.
Discuss Your Application →Tubes that carry acid on one side and cooling water on the other.
Tube-side and shell-side parts in dilute acid service.
Heating tubes in wet-process evaporator circuits.
Heating and cooling coils submerged in pickling baths.
Tubes that see chlorinated water with a low acid load.
Pipe specified under NACE MR0175 and ISO 15156-3.
Lines that carry acid and caustic during cleaning cycles.
Finally, ducting and spray headers exposed to acid condensate.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The limits below come from ASTM B463, B473, and B729, which share one composition table for UNS N08020. Copper is the deliberate addition behind the acid performance, and the niobium range scales with the carbon content. The mill certificate governs final acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 32.0–38.0% |
| Chromium (Cr) | 19.0–21.0% |
| Copper (Cu) | 3.0–4.0% |
| Molybdenum (Mo) | 2.0–3.0% |
| Niobium + Tantalum (Nb+Ta) | 8 × C min., 1.00% max. |
| Manganese (Mn) | 2.00% max. |
| Silicon (Si) | 1.00% max. |
| Carbon (C) | 0.07% max. |
| Phosphorus (P) | 0.045% max. |
| Sulfur (S) | 0.035% max. |
| Iron (Fe) | Balance |
The tubular documents set one stabilised annealed condition across both the seamless and the welded routes, so one row set covers the page. Two details separate the documents, and both appear underneath.
| Product Form | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation | Hardness |
|---|---|---|---|---|---|
| Seamless pipe and tube, ASTM B729 | Stabilised annealed | ≥80 ksi (550 MPa) | ≥35 ksi (240 MPa) | 30% | Not specified |
| Welded pipe, ASTM B464 | Stabilised annealed | ≥80 ksi (551 MPa) | ≥35 ksi (241 MPa) | 30% | Not specified |
| Welded tube, ASTM B468 | Stabilised annealed | ≥80 ksi (551 MPa) | ≥35 ksi (241 MPa) | 30% | Not specified |
The seamless document prints 80 and 35 ksi against 550 and 240 MPa, while the welded documents round those figures to 551 and 241 MPa. Still, we print each standard exactly as written rather than forcing one number set.
The welded pipe document reaches NPS 6 with Schedule 5S, 10S, and 40S, and it allows Schedule 80S up to NPS 2. It calls for automatic welding without filler metal, plus a flattening test on every lot. Beyond that size, we quote the wall by agreement.
The figures in this table are typical design values, and they are not acceptance limits. The alloy also stays non-magnetic, and instrument parts in acid circuits benefit.
| Property | Value |
|---|---|
| Density | Approx. 8.08 g/cm³ |
| Melting range | Approx. 1385–1443 °C |
| Modulus of elasticity | Approx. 193 GPa |
| Shear modulus | Approx. 76 GPa |
| Thermal conductivity at 20 °C | Approx. 12.3 W/m·K |
| Electrical resistivity at 20 °C | Approx. 1.08 µΩ·m |
| Specific heat at 20 °C | Approx. 500 J/kg·K |
| Thermal expansion, 25–100 °C | Approx. 14.7 µm/m·K |
| Magnetic response | Essentially non-magnetic |
| Strengthening route | Cold work only |
Four ASTM documents cover the tubular routes, and the ASME editions govern once a pressure code applies. In addition, no SAE aerospace specification reaches UNS N08020. The European and Chinese designations below serve cross-reference only.
| Standard | Product or Application |
|---|---|
| ASTM B729 / ASME SB729 | Seamless pipe and tube |
| ASTM B464 / ASME SB464 | Welded pipe |
| ASTM B468 / ASME SB468 | Welded tube |
| ASTM B366 / ASME SB366 | Factory-made wrought fittings for the same grade |
| NACE MR0175 / ISO 15156-3 | Sour service qualification for oil and gas |
| UNS N08020 | Unified Numbering System designation |
| W.Nr. 2.4660 / NiCr20CuMo | European designation |
| GB/T 15007 NS1403 | Chinese designation |
| SAE AMS | No aerospace specification covers this grade |
20Cb-3 and Carpenter 20 are trademarks of Carpenter Technology, and Incoloy is a trademark of Special Metals Corporation. We quote those names for reference only, and our deliveries follow the ASTM and ASME documents listed above.
The standard text from ASTM International settles any acceptance question.
Because each tubular document prints its own scope, the ranges below follow those texts rather than one house rule. For that reason, state the form and the ordered size on the enquiry.
| Product Form | Typical Supply Range |
|---|---|
| Seamless tube and pipe | Outside diameter 6–219 mm to ASTM B729 |
| Welded pipe | NPS 1/8 to 6 in Schedule 5S, 10S, and 40S to ASTM B464 |
| Welded pipe, light wall | NPS up to 2 in Schedule 80S to ASTM B464 |
| Welded tube | Outside diameter 3.2–88.9 mm to ASTM B468 |
| U-bend tube | Bent to the bundle drawing from seamless or welded stock |
| Coiled tube | Coil lengths quoted to the order |
Wall thickness runs from 0.5 mm up to 12 mm across the seamless range, and heavier wall moves to a quoted basis. Therefore, give the outside diameter and the wall on the enquiry so we price the right document.
Finish follows the operation that comes next rather than a catalogue default. In short, we agree the surface with your order.
| Surface Condition | Typical Use |
|---|---|
| Stabilised annealed and pickled | Standard delivery for acid and chloride service |
| Bright annealed | Scale-free bore for instrument and clean circuits |
| Cold drawn | Close wall control with a smoother bore and outside surface |
| Polished bore | Reduced roughness for product-contact hygienic lines |
| U-bend stress relieved | Bends annealed after forming for exchanger service |
Get detailed information including specifications, standards, dimensions and material properties.
Eight steps carry an enquiry from the first message to the delivered bundle. Therefore, send the duty and the size list first, and the rest follows.
State the acid, its concentration, the working temperature, and the pressure class.
Tell us whether the line needs seamless tube, welded pipe, or welded tube.
Outside diameter, wall, and length go on the enquiry in one table.
We agree hydrostatic, eddy current, or flattening checks against the standard and your specification.
Price, lead time, and the certificate package reach you together.
Grade, size, inspection level, and delivery terms go on the record.
The mill takes the lot through drawing, annealing, quenching, and release testing.
Finally, the desk follows the shipment and mails the paperwork before it lands.
Feedback from buyers and engineers who source nickel alloy materials from Southerly Alloy.
“The bundle arrived with the anneal chart attached, so the client's corrosion review closed in one session.”
“Seamless tube held its wall tolerance through the whole order, and the second batch matched the first.”
“In short, cooling coils in UNS N08020 replaced a 316L set and ran three campaigns without a leak.”
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B729 covers seamless pipe and tube, B464 covers welded pipe, and B468 covers welded tube.
Seamless tube runs from 6 to 219 mm outside diameter, with wall thickness from 0.5 up to 12 mm.
ASTM B464 prints its scope as NPS 6 with Schedule 5S, 10S, and 40S. Therefore, we quote larger sizes and heavier wall by agreement instead.
C-276 tolerates stronger acid and higher chloride levels, and it costs considerably more. Alloy 20 covers dilute acid duty at a lower price.
ER320LR for TIG and MIG, and E320LR for stick welding. Both are low-residual grades that resist hot cracking.
One length covers most stock sizes, and a short cut is enough for a trial.
We quote mainly on FOB terms, and EXW or CIF follow on request.
Price follows the outside diameter, the wall, the length, and the test level. We quote per metre or per piece on request.
Stock sizes ship in 7-15 days, and made-to-order tube runs about 25 days.
Yes. Every heat ships with an EN 10204 3.1 certificate, and we arrange 3.2 endorsement on request.
Give us the outside diameter, the wall thickness, and the medium. We answer with price, lead time, and the certificate package in one message. Because welded pipe stops at the schedule the standard prints, state the wall you need.
A short trial length costs very little, so one tube settles the question before a plant-wide order.