01
Hastelloy C-276 Seamless Pipe
Pressure and transfer lines to ASTM B622, in hot-finished or cold-finished condition.
Request Availability →Seamless and welded UNS N10276 tubular product to B622, B619, and B626 for acid, chloride, and wet-chlorine duty.
We quote B622 seamless product alongside B619 pipe and B626 tube under a single UNS N10276 enquiry.
Every welded length leaves the plant solution annealed and water quenched, so it meets the ordered document.
Moist chlorine, hypochlorite, and chlorine dioxide dissolve most metals, and tubular C-276 outlasts them all.
Hastelloy C-276 Pipe and Tube serves chemical and pollution-control lines where one process stream mixes oxidizing and reducing attack. Molybdenum and tungsten suppress reducing-acid and chloride attack while chromium covers oxidizing media. Each length follows B622, B619, or B626.
Grade-level data sits on the Hastelloy C-276 hub, and the two other forms are covered on the Hastelloy C-276 Bar and Rod and Hastelloy C-276 Plate and Sheet pages.
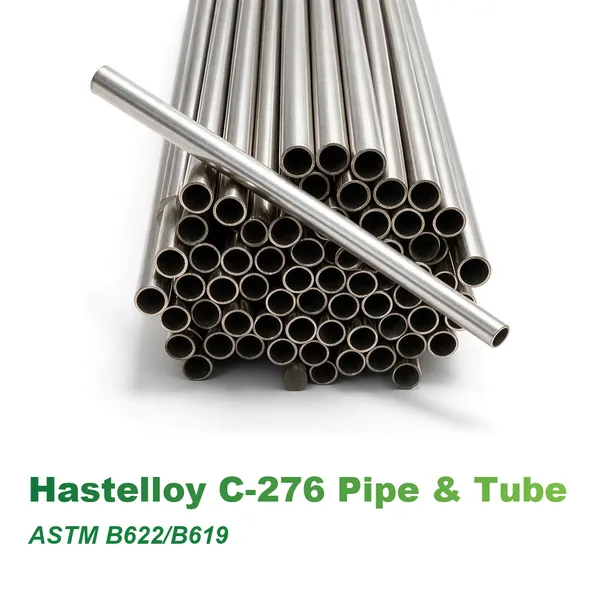
Hastelloy C-276 pipe and tube covers seamless product to ASTM B622 plus welded pipe to B619 and welded tube to B626, quoted against schedule, gauge, or drawing. Sizes run from small condenser tube to NPS 24 line pipe, supplied solution annealed and water quenched. Molybdenum and tungsten carry these lines through hydrochloric and sulphuric acid, wet chlorine, and chloride-bearing slurry. EN 10204 3.1 certificates and heat-level traceability back chemical, FGD, and sour-service projects.
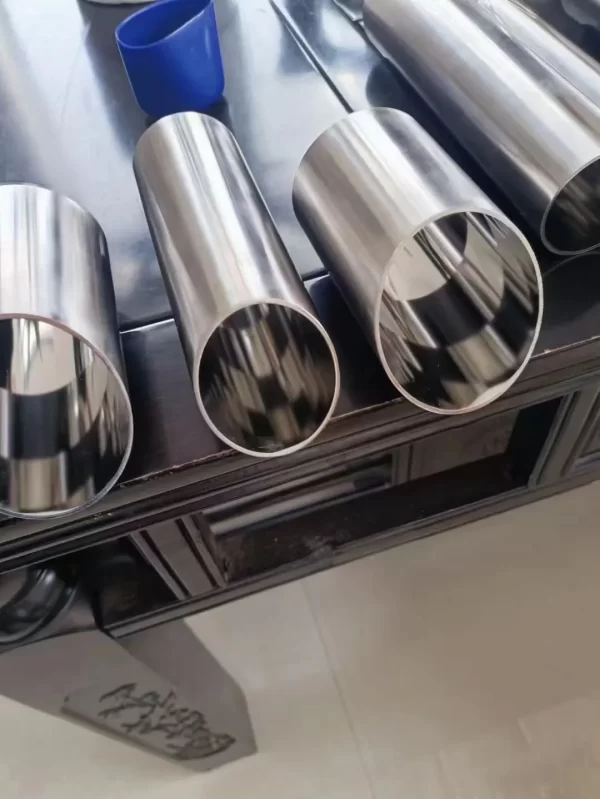
In addition, tubular product handles HCl across a wide concentration range, subject to each line's temperature limit.
Indeed, moist chlorine gas, hypochlorite liquor, and chlorine dioxide leave few metals intact.
Molybdenum at 15.0–17.0% keeps localised attack in check where seawater or chloride liquor wets the wall.
Chloride-induced stress-corrosion cracking does not trouble a nickel-rich matrix of this type.
Carbon at 0.010% max leaves the weld heat-affected zone free of grain-boundary precipitates.
Besides, B622 carries the ductility evidence that tube expansion into tubesheets requires.
Also, B626 welded tube passes 100% eddy-current or ultrasonic examination before release.
Meanwhile, process piping for H2S duty travels with NACE MR0175 / ISO 15156 hardness records.
For tubular work, Southerly Alloy keeps the commercial relationship while audited partner plants pierce, weld, and finish the tube. Your enquiry goes straight to the mill that runs that production route. Consequently, you settle condition and documentation questions in a single thread.
Pressure, diameter, medium, and budget fix the seamless or welded choice before the quotation leaves.
Condenser tube at 6 mm OD and line pipe at NPS 24 come from the same quotation desk.
Hydrostatic, eddy-current, PMI, and third-party inspection attach at purchase stage.
Packing, Incoterm, and export paperwork clear before dispatch.
Every UNS N10276 heat moves through melt, hot working, cold finishing, and a water-quenched anneal before release. In addition, the sequence shifts with the standard, gauge, and acceptance level on the order.
We weigh nickel, chromium, molybdenum, tungsten, and iron into the N10276 window before the melt begins.
VIM or AOD treatment holds carbon, silicon, and gas content inside the limits that protect weld zones.
Billets take a pierce or extrusion pass into seamless shells, while welded product starts from flat-rolled coil.
Cold pilgering or drawing brings condenser and precision tube down to final outside diameter and wall.
Material passes through 1120 to 1160 °C, then takes a rapid water quench that dissolves precipitates.
Welded lengths receive a matching ERNiCrMo-4 seam, then a full solution anneal and quench.
Our operators pickle and dimension-check each length, run hydrostatic or eddy-current tests, and release it against the ordered acceptance level.
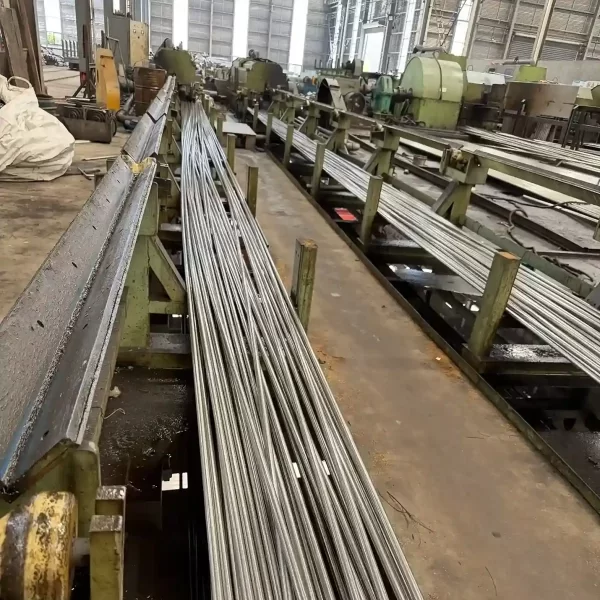
Seamless and welded UNS N10276 tube covers condenser sizes through heavy line pipe. We check every order against our rolling and annealing plan before production starts. Consequently, the plan confirmed at quotation is the plan that leaves the plant.
Melt shop, tube rolling line, and annealing hall share one site.
Pilgering, drawing, welding, and finishing equipment run under a single quality system.
Monthly tonnage of nickel alloy tubular product, from stock sizes to made-to-order.
Our metallurgists match the anneal and test scope to the medium before release.
We clear chemistry, mechanics, dimensions, and surface on every batch before release. That verification sits inside the ISO 9001 system. Above all, a 3.1 certificate accompanies each shipment, and we can book third-party inspection onto the order.
Spectrometry confirms the N10276 window, and our report prints carbon and silicon beside the molybdenum figure.
Tensile, yield, and elongation values come from the delivered condition and wall thickness.
We measure OD, wall, straightness, and finish, then add hydrostatic or eddy-current records where ordered.
The heat number on each certificate maps a length back to its melting charge.
Six tubular routes carry this grade, and each one follows its own standard and finishing sequence.
Pressure and transfer lines to ASTM B622, in hot-finished or cold-finished condition.
Request Availability →Condenser, exchanger, and evaporator tube to B622 with B829 general requirements.
Request Availability →Next, B619 pipe with a matching-filler seam, solution annealed after welding.
Request Availability →Likewise, B626 tube carries a tighter OD tolerance and 100% eddy-current examination.
Request Availability →Continuous coils and bespoke U-bends formed from B622 base stock.
Request Availability →Electropolished and bright annealed tube for pharmaceutical and high-purity circuits.
Request Availability →Tubular duty here follows the medium more than the pressure rating, because chloride and acid attack set the wall life. Accordingly, the services below pair each environment with the tube form that carries it.
Discuss Your Application →Spray headers, lance piping, and duct drains for limestone-gypsum slurry.
Transfer piping in bleach and disinfection plants.
Column internals, reboiler tube, and transfer lines for hydrochloric acid service.
Exchanger tube for concentrated acid streams at elevated temperature.
For example, tube circuits in once-through and offshore cooling systems.
In addition, gathering and treatment lines for H2S-bearing production.
Chlorine dioxide and washer circuits in pulp and paper mills.
Electropolished tube for clean chemical and API duty.
Finally, tube bundles for wet-process acid concentration trains.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The window below covers the B622, B619, and B626 tubular family for UNS N10276. Molybdenum and tungsten drive reducing-acid and chloride resistance, chromium carries oxidizing duty, and carbon stays ultra-low to protect welded seams. However, the purchase specification in force decides acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 57.0% min. (balance) |
| Molybdenum (Mo) | 15.0–17.0% |
| Chromium (Cr) | 14.5–16.5% |
| Tungsten (W) | 3.0–4.5% |
| Iron (Fe) | 4.0–7.0% |
| Cobalt (Co) | 2.50% max. |
| Manganese (Mn) | 1.00% max. |
| Vanadium (V) | 0.35% max. |
| Silicon (Si) | 0.08% max. |
| Carbon (C) | 0.010% max. |
| Phosphorus (P) | 0.040% max. |
| Sulphur (S) | 0.030% max. |
Minimum room-temperature values below follow the governing standard and the solution-annealed condition. Therefore, name the ASTM document and the ordered wall thickness at enquiry so acceptance is unambiguous.
| Product Form | Standard | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation |
|---|---|---|---|---|---|
| Seamless pipe and tube | ASTM B622 | Solution annealed | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Welded pipe | ASTM B619 | Solution annealed after welding | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
| Welded tube | ASTM B626 | Solution annealed after welding | ≥690 MPa (100 ksi) | ≥283 MPa (41 ksi) | ≥40% |
B622 adds hydrostatic, flattening, and flare tests to seamless product. B626 brings a 100% eddy-current or ultrasonic examination, which suits exchanger duty. Meanwhile, no dedicated AMS document covers C-276 tubular product, so aerospace tube follows the project specification or the ASTM document named on the order.
| Property | Value |
|---|---|
| Alloy | Hastelloy C-276 |
| UNS | N10276 |
| Werkstoff | 2.4819 |
| Density | Approx. 8.89 g/cm³ |
| Melting Range | Approx. 1325–1370 °C |
| Elastic Modulus | Approx. 205 GPa |
| Thermal Conductivity | Approx. 10.2 W/m·°C at 20 °C |
| Specific Heat | Approx. 427 J/kg·°C |
| Expansion Coefficient | Approx. 11.2 µm/m·°C (20–100 °C) |
| Alloy Type | Nickel-molybdenum-chromium with tungsten |
| Standard | Product / Application |
|---|---|
| ASTM B622 / ASME SB622 | Seamless pipe and tube, cold-finished or hot-finished |
| ASTM B619 / ASME SB619 | Welded pipe, solution annealed after welding |
| ASTM B626 / ASME SB626 | Welded tube for heat exchangers, condensers, and evaporators |
| ASTM B829 | General requirements for seamless nickel alloy pipe and tube |
| ASTM B775 / B751 | General requirements for welded nickel alloy pipe and tube |
| ASME B16.25 | Buttwelding ends |
| NACE MR0175 / ISO 15156 | Sour service in oil and gas production |
| DIN 17751 | Nickel alloy tube, W.Nr. 2.4819 |
| ISO 6207 | Nickel alloy seamless tube |
| UNS N10276 · W.Nr. 2.4819 · NiMo16Cr15W · NS334 | Designations |
The tubular documents come from ASTM International. In addition, pressure-code projects file against the ASME SB edition instead of the ASTM original.
B619 and B626 both require a solution anneal and water quench after welding, because the as-welded condition satisfies neither document.
| Product Form | Typical Supply Range | Length |
|---|---|---|
| Seamless pipe | NPS 1/2 to NPS 24, SCH 5S to XXS | Single random, double random, or custom |
| Seamless tube | OD 6.35–114.3 mm, wall 0.5–10 mm | Up to 12 m or custom cut lengths |
| Heat-exchanger tube | OD 6.35–76.2 mm, wall 0.7–6 mm | Up to 12 m or U-bend |
| Welded pipe | OD 21.3–610 mm, wall 0.5–100 mm | Fixed length or random |
| Welded tube | OD 3.18–127 mm, wall 0.38–12.7 mm | Coil or fixed length |
| EP / BA tube | OD 6–50.8 mm, wall 0.5–3 mm | Up to 6–12 m, clean service |
Windows beyond the listed range depend on billet and coil supply. Therefore, quote the OD, wall, length, condition, and end finish so the route and price can be fixed.
| Surface Condition | Typical Characteristics / Applications |
|---|---|
| Solution Annealed & Pickled | Standard delivered condition for acid and chloride service |
| Bright Annealed | Smooth, scale-free bore and OD for instrumentation and clean circuits |
| Pickled Only | Acid-descaled surface for general chemical piping |
| Beveled End | Weld-preparation beveling to the agreed standard for butt welds |
Get detailed information including specifications, standards, dimensions and material properties.
A tubular order usually ships two to four weeks after release, though heavy-wall welded pipe takes longer. Before the price is fixed, the steps below line up standard, condition, and test scope with your duty.
Give the OD, wall, length, quantity, and ordered condition, plus the medium and its concentration.
Seamless work runs to B622, welded pipe to B619, and welded tube to B626.
Welded lengths always take a solution anneal after welding, and seamless product ships annealed as standard.
Your quotation states price, route, test scope, documentation, and Incoterm together.
The plant manufactures and tests to the acceptance level agreed at order placement.
Every consignment travels with its 3.1 certificates, packing list, and export papers.
Feedback from buyers and engineers who source nickel alloy materials from Southerly Alloy.
“The B622 exchanger tube arrived with flare and flattening records attached, so our expansion trial ran without a re-test.”
“Seawater condenser tube held its wall tolerance across the full bundle order, and the heat numbers matched our inspection file.”
“Replacement pipe for our HCl recovery line carried the post-weld anneal record, which our insurer asked to see.”
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
Seamless pipe and tube are ordered to ASTM B622, while welded pipe follows B619 and welded tube follows B626. Under code jurisdiction the ASME SB editions apply.
Yes. B619 and B626 both require a full solution anneal and water quench after welding. For that reason, we do not quote as-welded pipe as standard-compliant product.
Supplier data documents continuous air service to roughly 540 °C. However, the medium, its concentration, and the pressure rating usually set the real ceiling, so confirm the duty at enquiry.
Welded tube to B626 runs from OD 3.18 mm to 127 mm, with walls from 0.38 mm to 12.7 mm. Larger or heavier sections come from a separate quote.
Sour-service orders run to NACE MR0175 / ISO 15156 with per-heat hardness records. Therefore, upstream projects can file the evidence their material review needs.
Stock sizes ship 7-15 days, while made-to-order and heavy-wall product runs against the confirmed production schedule.
One piece covers many stock sizes, so trial lengths and repair pieces carry no premium hurdle.
FOB is the default Incoterm, while EXW, CIF, and DAP quotes follow confirmed destinations.
Pricing follows the ordered size, wall, and condition, and we normally calculate it by weight in kilograms. We confirm the applicable Incoterm on the offer.
Yes. Every delivery carries an EN 10204 3.1 certificate, and we arrange third-party 3.2 endorsement on request.
Send the OD, wall, length, standard, and quantity, and we reply with price, Incoterm, lead time, and document list. Medium and test-scope questions can ride along in the same message.