01
Hastelloy C-276 Round Bar
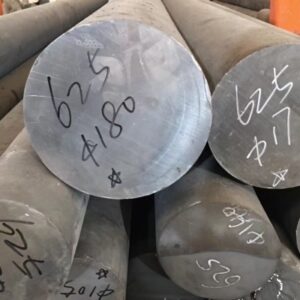
Solid rounds from 6 to 340 mm serve chlorine-compressor shafts, hydrochloric pump shafts and scrubber agitators.
View Hastelloy C-276 Round Bar →Proven nickel-chromium-molybdenum-tungsten bar and rod for severe corrosion, chloride, and sour-service duty where standard alloys fail.
We print the ultra-low carbon and silicon results that protect weld zones on every EN 10204 3.1 certificate. Therefore, your welders can verify the chemistry before they start.
We record the anneal and water-quench route used for your bar on the release document. In addition, the lot number ties every test back to its heat.
Because NACE MR0175 / ISO 15156 orders need proof, we ship them with hardness data keyed to each heat number.
Hastelloy C-276 bar and rod arrive in UNS N10276 (W.Nr. 2.4819), the nickel-chromium-molybdenum-tungsten alloy with ultra-low carbon. Because its chemistry is balanced, the grade resists oxidizing and reducing acids, chloride pitting, crevice corrosion, and stress-corrosion cracking.
As a Hastelloy C-276 bar supplier we hold round, hex, square and forged sections in solution-annealed, hot-worked and cold-drawn conditions, all certified to ASTM B574 and ASME SB574. Next, we cut every lot to order and release it with an EN 10204 3.1 certificate. Meanwhile, where service needs higher strength at temperature than C-276 provides, our Inconel 625 bar and rod extends the nickel-alloy range.

Hastelloy C-276 is a nickel-chromium-molybdenum-tungsten alloy with ultra-low carbon that resists oxidizing and reducing acids, chloride pitting, crevice corrosion, and stress-corrosion cracking. Southerly Alloy supplies UNS N10276 bar and rod to ASTM B574 in solution-annealed, hot-finished, and cold-drawn conditions, with custom sizes, surface finishes, and EN 10204 3.1 mill test certificates. Because of this, chemical plants, pollution-control systems, and sour-service oil and gas projects typically specify this bar.

For example, chromium, molybdenum, and tungsten together handle nitric, sulfuric, hydrochloric, and mixed-acid streams.
Similarly, its high molybdenum content resists localised attack in seawater and chloride process streams.
In addition, the nickel-rich matrix stays immune to chloride-induced SCC across the working range.
Because carbon and silicon stay ultra-low, welded joints remain corrosion-resistant without post-weld heat treatment.
After hot working and forming, a water-quenched anneal restores full corrosion resistance.
Therefore, C-276 meets NACE MR0175 / ISO 15156 within the applicable hardness limits for H2S duty.
Over five decades of service have made it the default choice where failure is not an option.
As a result, each bar leaves with an EN 10204 3.1 certificate that names its heat number.
C-276 bar earns its place where one stream carries oxidizing and reducing attack at once. Besides, we confirm the carbon and silicon limits, the anneal and the hardness basis with you before we book the heat. Heat-specific chemistry records travel with the material certificate.
We check carbon, silicon, and molybdenum targets against your specification before we pour the heat.
We compile certificates, hardness records, and PMI data per heat, and they follow the bar to site.
Because one test bar and a full order run through the same solution-annealed route, you see the result before the container.
Our mill metallurgists, who set the anneal, answer your acid, chloride, and sour-service questions directly.
We begin each C-276 bar as a vacuum-refined melt and hold carbon and silicon low to protect weld zones. Next, we solution-anneal and water-quench each heat, then finish to the ordered condition. Finally, we file chemistry and test data against the heat number through release.
We weigh nickel, chromium, molybdenum, tungsten, and iron into the UNS N10276 window before melting.
We refine the charge under vacuum or argon to keep carbon, silicon, and gas within limits.
We forge and roll the ingots down to bar section, and this breaks the cast structure as the size reduces.
We heat the bar above 1100 °C and rapidly water-quench it to dissolve precipitates and restore corrosion resistance.
We draw, peel, or centreless-grind the bars to the ordered diameter, tolerance, and surface.
We straighten and cut the bars to length, and we agree the machining allowance for further turning.
We remove scale by pickling or grinding so the surface stays clean for acid and seawater duty.
We check chemistry, tensile, hardness, and dimensions against the ordered condition before release.
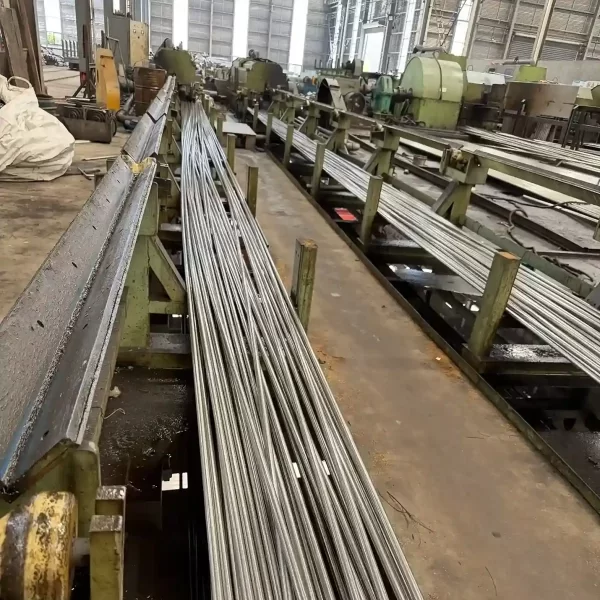
We produce C-276 bar in stock and made-to-order diameters, fixing the solution-annealed condition before cutting. Overall, the numbers below show the melting, annealing and test capacity behind that promise. In addition, acid-duty and sour-service work shares the same qualified route.
Integrated melting, annealing, and finishing lines run under one roof.
This equipment handles hot working, solution annealing, drawing, and grinding.
We output this much nickel-corrosion-alloy bar across stock and order-specific diameters each month.
These metallurgists review your chloride and sour-service specifications with you.
C-276 bar can be supplied for sour-service applications in accordance with NACE MR0175 / ISO 15156, with heat-specific hardness and chemical composition records available when required by the order.
No C-276 bar leaves the works until we prove the ordered ASTM B574 requirements on the heat. First, we check carbon and silicon by spectrometer against the N10276 window. Then we record tensile, hardness, and intergranular results where your specification asks for them.
We measure carbon, silicon, and molybdenum per heat and check them against the ASTM B574 limits.
We record tensile and hardness results for the condition actually shipped, not a generic value.
We measure diameter, straightness, and finish to the B574 tolerance class, with PMI where specified.
In addition, certificates carry the heat number, so you can trace any bar to its test results at incoming inspection.
Round bar and rod carry most C-276 enquiries, and each condition below has a page of its own. Meanwhile, those twelve pages set out the sections, tolerances and document route for each form. Therefore, we agree the machining allowance with the order.
Solid rounds from 6 to 340 mm serve chlorine-compressor shafts, hydrochloric pump shafts and scrubber agitators.
View Hastelloy C-276 Round Bar →Smaller drawn stock with controlled straightness fits pins, instrument studs and fixture work.
View Hastelloy C-276 Round Rod →A bright-drawn, peeled or ground finish suits automatic lathes turning chlorine-plant parts.
View Hastelloy C-276 Bright Bar →Higher yield from the as-drawn condition, straightened where a tight runout matters.
View Hastelloy C-276 Cold-Drawn Bar →Sections sized across flats serve moist-chlorine flange nuts and NACE-documented bolting.
View Hastelloy C-276 Hex Bar →Squares cut to width and length carry scrubber duct frames and hydrochloric skid structures.
View Hastelloy C-276 Square Bar →Rectangular sections to specified thickness and width serve absorber internals and duct stiffeners.
View Hastelloy C-276 Flat Bar →Larger diameters and shaped sections with a controlled wrought structure suit heavy valve bodies.
View Hastelloy C-276 Forged Bar →Ground diameter and straightness held for scrubber pump spindles and acid metering plungers.
View Hastelloy C-276 Centreless-Ground Rod →Fully threaded bar and studs cut from B574 stock, with F468 coverage and hardness records for NACE orders.
View Hastelloy C-276 Threaded Rod →Fine and spring-temper wire to DIN 17753 for demister pads, filtration mesh and springs.
View Hastelloy C-276 Wire →ERNiCrMo-4 bare wire and ENiCrMo-4 electrodes that carry the corrosion resistance of the parent metal.
View Hastelloy C-276 Welding Wire →Engineers specify C-276 bar where one alloy must survive oxidizing and reducing attack in the same stream. Most of this bar goes to chemical plants, sour-service oil and gas, and pollution control. Therefore, tell us the medium, concentration, and temperature when you request a quote.
Discuss Your Application →For example, we supply pump shafts, valve stems, and agitator shafts for HCl production, storage, and handling.
In addition, we supply reactor internals, mixer shafts, and fittings across wide acid concentrations.
Similarly, because they resist pitting, we supply tubesheet, baffle and support parts for seawater-cooled exchangers.
We supply wellhead, tree and valve components for H2S-bearing duty within NACE limits.
In FGD systems, we supply scrubber spray headers, dampers, and duct supports for aggressive environments.
Because the duty is aggressive, we supply hardware for acidic combustion products and wastewater streams.
We supply agitator shafts and baffle supports where metallic contamination must stay low.
In pulp and paper, we supply digester fittings, bleach-plant hardware, and blow-line parts for chlorine-bearing service.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The limits below follow ASTM B574 for UNS N10276 bar and rod, with nickel as the balance of the melt. Molybdenum and tungsten set the reducing-acid and localised-corrosion resistance; in contrast, chromium covers oxidizing media and ultra-low carbon protects the weld zones. Therefore, the mill test certificate governs final acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 57.0% min. (balance) |
| Chromium (Cr) | 14.5–16.5% |
| Molybdenum (Mo) | 15.0–17.0% |
| Tungsten (W) | 3.0–4.5% |
| Iron (Fe) | 4.0–7.0% |
| Cobalt (Co) | 2.5% max. |
| Manganese (Mn) | 1.0% max. |
| Vanadium (V) | 0.35% max. |
| Silicon (Si) | 0.08% max. |
| Carbon (C) | 0.010% max. |
| Phosphorus (P) | 0.040% max. |
| Sulfur (S) | 0.030% max. |
Values below separate the ASTM B574 minimums from results typically measured on solution-annealed bar. Moreover, the standard sets one condition for rod and bar, and its Table 5 carries no hardness requirement. Therefore, we agree any hardness ceiling with the order.
| Condition | Tensile Strength | Yield Strength (0.2%) | Elongation | Hardness |
|---|---|---|---|---|
| Annealed — ASTM B574 minimum | ≥100 ksi (690 MPa) | ≥41 ksi (283 MPa) | 40% | No requirement in Table 5 |
| Annealed bar — typical values | 115 ksi (790 MPa) | 55 ksi (380 MPa) | 50% | Approx. 90 HRB (100 HRB commonly reported) |
C-276 is not age-hardenable, so any strength above the annealed minimum comes from cold work. We quote cold-drawn bar to its as-drawn condition when a higher yield is needed.
Typical room-temperature values below support design work rather than acceptance testing. Moreover, since C-276 stays practically non-magnetic across its working range, it suits instrument and magnetically sensitive assemblies.
| Property | Value |
|---|---|
| Density | Approx. 8.89 g/cm³ |
| Melting range | Approx. 1325–1370 °C |
| Modulus of elasticity | Approx. 205 GPa |
| Thermal conductivity at 20 °C | Approx. 10.2 W/m·K |
| Specific heat at 20 °C | Approx. 427 J/kg·K |
| Electrical resistivity at 20 °C | Approx. 1.30 µΩ·m |
| Thermal expansion, 20–100 °C | Approx. 11.2 µm/m·K |
| Magnetic behaviour | Practically non-magnetic at ambient temperature |
ASTM B574 governs bar and rod, and ASME SB574 covers pressure equipment. The designations below are cross-reference identifiers rather than separate approvals. In addition, sour-service orders reference NACE MR0175 / ISO 15156, subject to the applicable hardness limits. ASTM International publishes these documents, and the ASME SB editions govern once equipment falls under pressure-code jurisdiction.
| Standard / Designation | Scope |
|---|---|
| ASTM B574 | Nickel-chromium-molybdenum-tungsten alloy rod and bar — UNS N10276 among eleven grades |
| ASME SB574 | ASME edition for rod and bar |
| ASTM B564 / ASME SB564 | Nickel alloy forgings — UNS N10276 |
| ASTM B462 | Flanges, forged fittings and valve parts in the same grade |
| ASTM F468 | Bolts, hex cap screws, socket head cap screws and studs in UNS N10276 |
| ASTM B575 / ASME SB575 | Plate, sheet, and strip in the same grade |
| ASTM B622 / ASME SB622 | Seamless pipe and tube in the same grade |
| NACE MR0175 / ISO 15156 | Sour service in oil and gas production |
| UNS N10276 | Material designation for Hastelloy C-276 |
| W.Nr. 2.4819 / NiMo16Cr15W | European designation for Alloy C-276 |
| DIN 17752 / DIN 17753 / DIN 17754 | Wrought nickel alloys — bar, wire, and forging stock |
| AMS 5750 | Aerospace bars, forgings and flash-welded rings in UNS N10276 |
| ISO 9723 / ISO 9724 / ISO 9725 | Nickel alloy bar, wire, and forging stock |
| VdTÜV 400 | German pressure vessel material data sheet |
Ranges below reflect normally produced sections; exact availability depends on condition, finish, and quantity, confirmed at quotation. However, we assess non-standard diameters and lengths against the mill route before we return a quotation.
| Product Form | Typical Supply | Length |
|---|---|---|
| Round Bar | 6–340 mm dia. | Cut to length or random |
| Round Rod | 3–50 mm dia. | Cut to length |
| Bright Bar | 6–150 mm dia. | Cut to length or random |
| Square Bar | 10–150 mm | Cut to length or random |
| Hex Bar | 10–150 mm A/F | Cut to length or random |
| Flat Bar | 3–100 mm thick × 10–300 mm wide | Cut to length |
| Forged Bar | 100–340 mm dia. or forged section | Cut to length |
| Precision-Ground Rod | 3–100 mm dia., tight tolerance | Cut to length |
We choose each finish for the next operation, whether machining allowance, acid-service exposure, or a painted assembly. Availability depends on diameter, condition, and order quantity. Therefore, we agree each finish with the order rather than assume it from stock.
| Surface Condition | Typical Use |
|---|---|
| Solution annealed and pickled | Standard delivery for acid and seawater service |
| Hot-worked (as-rolled or forged) | Parts that will be machined to size |
| Cold drawn | Close diameter control with a brighter surface |
| Peeled | Uniform diameter with a machined skin for further turning |
| Centreless ground | Tight diameter and straightness for shafting |
| Polished | Reduced roughness for product-contact and visible parts |
| Rough turned | Machining allowance held on large or forged bar |
Get detailed information including specifications, standards, dimensions and material properties.
One coordinator keeps your C-276 order moving from enquiry to shipment. Meanwhile, our technical team reviews acid or sour duty early, because we fix the solution-anneal route before we cut the bar.
Share the medium, its concentration and temperature, plus the diameter, length, and quantity.
Next, we agree the annealed, hot-finished, or cold-drawn condition with your machining plan.
After that, a single reply returns the price, lead time, and document list.
You approve the dimensions, inspection level, and delivery terms in writing before we begin cutting.
We then work, solution-anneal, and test your bar to the ordered condition.
Finally, the bar ships with its certificates and export documents, and we confirm the delivery terms with you.
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B574 / ASME SB574.
Yes. We supply it across a wide range of hydrochloric acid concentrations, subject to temperature limits.
Yes. We supply it to NACE MR0175 / ISO 15156, and we record hardness per heat within the applicable limits.
6–340 mm round bar, with rod from 3 mm and hex, square, and flat sections to 150 mm.
Yes. Peeling, grinding, and cut-to-length services cover diameters outside our stock range.
One bar for most stock diameters.
Mainly FOB; EXW and CIF can be quoted as well.
Mainly on weight; we fix the nickel, molybdenum, and tungsten share in the quotation.
7-15 days for stock sizes; about 25 days for made-to-order annealed bar.
Yes. 3.1 comes with every heat; we arrange 3.2 and third-party witness on request.
Send the medium, concentration, and dimensions, and we quote stock or custom C-276 bar with price, lead time, and documents. Moreover, we fix the anneal and inspection level before production, so the bar we approve is the bar that ships.