01
Inconel 600 Seamless Pipe
Hot-worked and cold-worked annealed pipe to ASTM B167 for pressure and furnace lines.
View Inconel 600 Seamless Pipe →UNS N06600 seamless and welded pipe and tube to B167, B163, B517, and B516 for furnace, caustic, and exchanger duty.
Precision tube through large-diameter furnace pipe is quoted under one UNS N06600 inquiry.
Lines run annealed for forming work or as-worked where strength matters most.
Chemistry, mechanical, and traceability records are compiled for nuclear and caustic review.
Inconel 600 Pipe and Tube is supplied in UNS N06600, a nickel-chromium-iron alloy built for oxidation and caustic duty. Meanwhile, chloride stress-corrosion cracking stays off the risk list in furnace and alkaline service. Each length is quoted from B167, B163, B517, or B516.
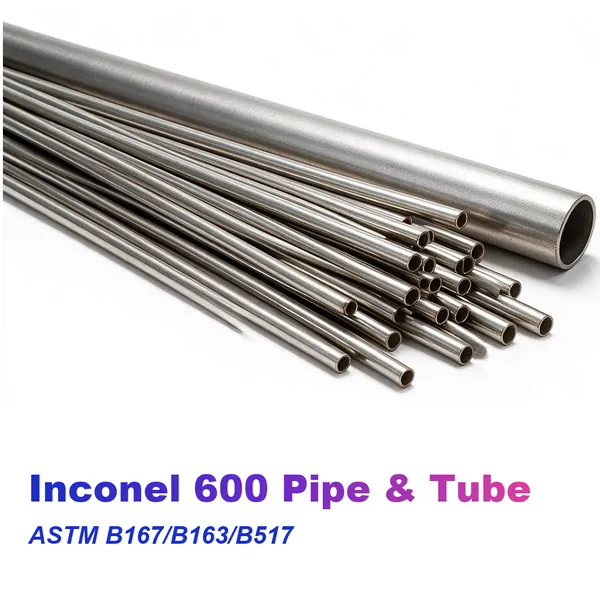
Southerly Alloy supplies UNS N06600 seamless pipe and tube to ASTM B167 and B163, with welded pipe to B517 and welded tube to B516 quoted against schedule or drawing. Sizes run from precision instrumentation tube to large-diameter furnace piping, delivered annealed or as-worked. EN 10204 3.1 certificates and heat-level traceability support furnace builders, caustic processors, and nuclear review.
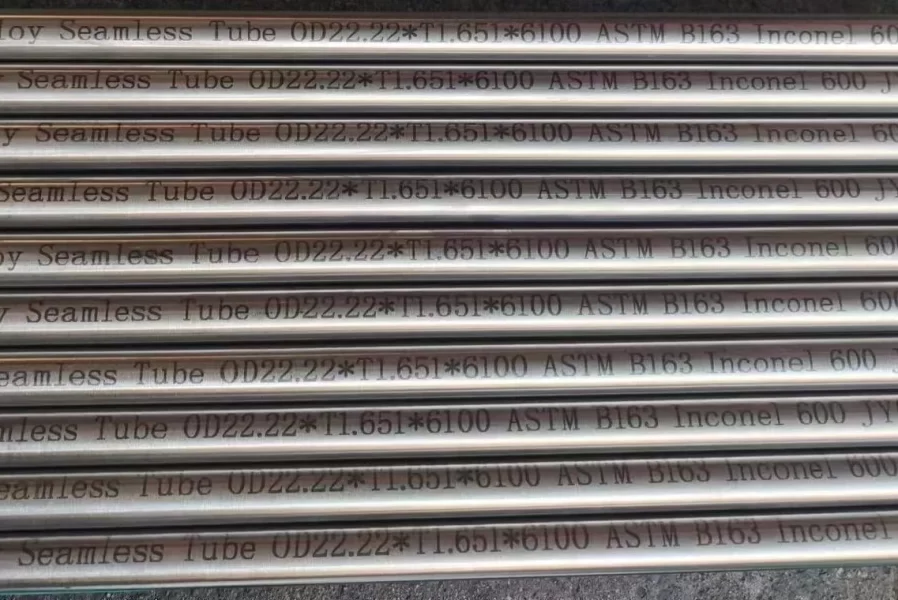
Furnace thermal cycling leaves the chromium oxide scale protective and intact.
NaOH and KOH evaporator systems run without the stress-corrosion cracking seen in stainless lines.
Stress-corrosion cracking from chloride ions stays off the risk list at this nickel level.
B167 and B163 cover seamless product, while B517 and B516 cover welded pipe and tube.
Halogen piping at elevated temperature is a documented Inconel 600 application.
Tubing keeps full ductility down to cryogenic temperature, so purge and cold lines stay safe.
EN 10204 3.1 certificates tie every pipe and tube shipment to its melting heat.
Tubular orders are coordinated by Southerly Alloy and executed at audited partner plants that melt and finish this grade. Your enquiry reaches the plant responsible for melting and finishing the pipe. Therefore, condition, size, and documentation decisions move in one conversation from inquiry to shipment.
Seamless or welded manufacturing is chosen against pressure, diameter, and budget before quotation.
Precision instrumentation tube through NPS 24 furnace piping runs from the same supplier base.
Hydro, NDT, PMI, and third-party inspection are attached to the order as the service requires.
Packing, Incoterm choice, and destination paperwork follow the shipment plan you confirm.
UNS N06600 tubular product follows a controlled route from melt to finished pipe. Also, the steps below flex to meet the ordered standard, condition, and acceptance level.
Nickel, chromium, and iron charge are weighed to the N06600 window and vacuum induction melted.
ESR or VAR refining improves cleanliness for nuclear and aerospace-bound heats.
Billets are hot extruded or hot pierced into seamless shells; plate is formed and welded for B517/B516 product.
Cold pilgering or drawing brings precision tube to final OD and wall with tight tolerances.
Furnace annealing between 900 and 1050 °C restores the soft condition before pickling.
Pipes and tubes are pickled, dimension-checked, and tested to the ordered acceptance level.
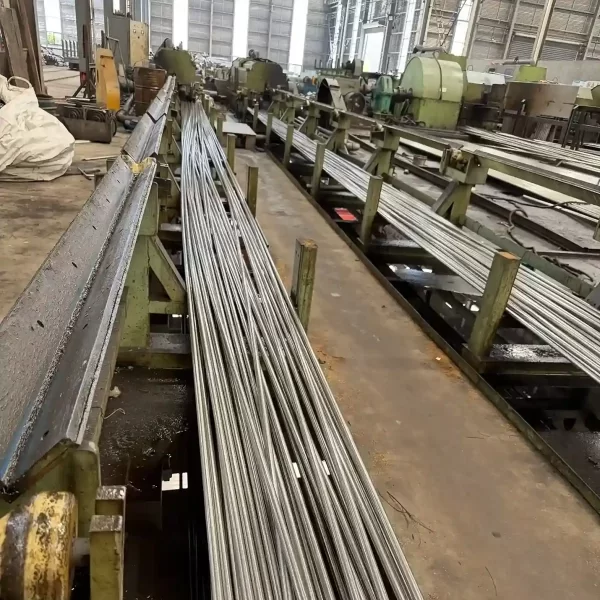
Seamless and welded Inconel 600 tubular product spans NPS 1/8 furnace pipe down to small-bore instrumentation tube. Diameter, wall, length, condition, and end finish are confirmed against your purchase requirements before production. As a result, the routing quoted at inquiry is the routing that runs.
Dedicated nickel-alloy workshops cover the complete tubular route.
Extrusion, pilgering, welding, and finishing lines share one quality system.
Seamless and welded nickel alloy output across standard and custom sizes.
Routing, condition, and acceptance decisions are settled before the order.
Every tubular batch passes the ordered acceptance checks before release, covering chemistry, mechanics, dimensions, and surface under the ISO 9001 system. Above all, an EN 10204 3.1 certificate travels with every shipment, and third-party inspection joins the order on request.
Spectrometer readings are checked against the UNS N06600 limits for every heat.
Tensile, yield, and elongation are confirmed on the ordered condition and size band.
OD, wall, straightness, and surface are examined, with hydro or ET as specified.
Heat-number traceability backs the EN 10204 3.1 certificate on every shipment.
Six tubular forms cover the UNS N06600 pipe and tube range. Each form follows its own ASTM standard and finishing route.
Hot-worked and cold-worked annealed pipe to ASTM B167 for pressure and furnace lines.
View Inconel 600 Seamless Pipe →Heat-exchanger and instrumentation tube to ASTM B163 and B829.
Request Availability →Longitudinal automatically welded pipe to ASTM B517 for large diameters.
Request Availability →Precision welded tube to ASTM B516 for heat-transfer equipment.
Request Availability →Continuous coil and custom U-bends for exchanger fabrication from B163 base material.
Request Availability →Electropolished and bright annealed tube for high-purity chemical systems.
Request Availability →Tubular duty here is governed by heat and alkali, while chloride pitting sits lower on the threat list. For that reason, the applications below pair oxidation or caustic performance with the temperature each system carries.
Discuss Your Application →Hardware operating between 800 and 1100 °C in oxidizing atmospheres.
NaOH and KOH concentration lines where stainless steels suffer stress-corrosion cracking.
Piping for dry chlorine and hydrogen chloride at elevated temperature.
Tubing above 600 °C where oxidation resistance governs the choice.
Cracking and reforming service with cyclic thermal stress.
Reactor-adjacent tubing qualified for high-purity water service.
Piping under repeated heat-up and cool-down with stability demands.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The chemistry window below is common to the B167, B163, B517, and B516 tubular family for UNS N06600. However, the governing purchase specification takes precedence for acceptance.
| Element | Content |
|---|---|
| Nickel (Ni) | 72.0% min. |
| Chromium (Cr) | 14.0–17.0% |
| Iron (Fe) | 6.0–10.0% |
| Carbon (C) | 0.15% max. |
| Manganese (Mn) | 1.00% max. |
| Silicon (Si) | 0.50% max. |
| Sulfur (S) | 0.015% max. |
| Copper (Cu) | 0.50% max. |
Minimum room-temperature values below follow the governing standard, condition, and size band. Therefore, the applicable ASTM condition must be specified for final acceptance.
| Product Form | Standard | Condition | Tensile Strength | Yield Strength, 0.2% Offset | Elongation |
|---|---|---|---|---|---|
| Seamless pipe and tube | ASTM B167 | Hot-worked annealed, ≤127 mm OD | ≥550 MPa (80 ksi) | ≥205 MPa (30 ksi) | ≥35% |
| Seamless pipe and tube | ASTM B167 | Hot-worked annealed, over 127 mm OD | ≥515 MPa (75 ksi) | ≥170 MPa (25 ksi) | ≥35% |
| Seamless pipe and tube | ASTM B167 | Cold-worked annealed, ≤127 mm OD | ≥550 MPa (80 ksi) | ≥240 MPa (35 ksi) | ≥30% |
| Seamless pipe and tube | ASTM B167 | Cold-worked annealed, over 127 mm OD | ≥550 MPa (80 ksi) | ≥205 MPa (30 ksi) | ≥35% |
| Heat-exchanger tube | ASTM B163 | Annealed | ≥552 MPa (80 ksi) | ≥241 MPa (35 ksi) | ≥30% |
| Welded pipe | ASTM B517 | As-welded or annealed | ≥550 MPa (80 ksi) | ≥240 MPa (35 ksi) | ≥30% |
| Welded tube | ASTM B516 | As-welded or annealed | ≥550 MPa (80 ksi) | ≥240 MPa (35 ksi) | ≥30% |
Aerospace AMS 5580 deliveries carry condition-specific minimums and extra process controls. Confirm the required condition at inquiry so the correct standard is quoted.
Buyers often weigh Inconel 600 against Inconel 625, because both are nickel-base tubular alloys yet they serve different threats. The table below separates the two so the line can be specified against its real governing environment.
| Property / Feature | Inconel 600 (UNS N06600) | Inconel 625 (UNS N06625) |
|---|---|---|
| Governing Standard | ASTM B167 / B163 / B517 / B516 | ASTM B444 / B705 / B704 |
| Primary Strength | High-temperature oxidation and caustic resistance | Chloride, seawater, and pitting resistance |
| Service Temperature | Continuous duty up to about 1093 °C | Continuous duty up to about 982 °C |
| Corrosion Focus | Caustic alkali, oxidation, dry chlorine | Seawater, chlorides, crevice and pitting attack |
| Alloying Cost Basis | Ni-Cr-Fe, no molybdenum | Ni-Cr-Mo-Nb with 8–10% Mo |
| Typical Tubular Duty | Furnace tubes, caustic evaporators, dry halogen lines | Offshore, seawater cooling, acid service lines |
| Property | Value |
|---|---|
| Alloy | Inconel 600 |
| UNS | N06600 |
| Werkstoff | 2.4816 |
| Density | Approx. 8.47 g/cm³ |
| Melting Range | Approx. 1370–1413 °C |
| Elastic Modulus | Approx. 214 GPa |
| Thermal Conductivity | Approx. 14.8 W/m·°C at 20 °C |
| Expansion Coefficient | 13.3 µm/m·°C (20–100 °C) |
| Alloy Type | Nickel-chromium-iron |
| Standard | Product / Application |
|---|---|
| ASTM B167 / ASME SB167 | Seamless pipe and tube, hot-worked and cold-worked |
| ASTM B163 / ASME SB163 | Seamless condenser and heat-exchanger tube |
| ASTM B517 / ASME SB517 | Welded pipe |
| ASTM B516 / ASME SB516 | Welded tube |
| ASTM B829 | General requirements for seamless nickel alloy pipe and tube |
| SAE AMS 5580 | Seamless tube and custom tubing |
| DIN 17751 | Nickel alloy pipe and tube, W.Nr. 2.4816 |
| ISO 6207 | Nickel alloy seamless tube |
| UNS N06600 · W.Nr. 2.4816 · NiCr15Fe | Designations |
ASTM publishes the governing documents at ASTM International, and the ASME counterpart applies once the line falls under code jurisdiction. Additionally, chlorine-system designers should confirm dry-gas limits against the process data for each project.
| Product Form | Typical Supply Range | Length |
|---|---|---|
| Seamless pipe | NPS 1/8 to NPS 24, SCH 10 to SCH 160 / XXS | Single Random, Double Random or Custom |
| Seamless tube | OD 6–101.6 mm, wall 0.5–10 mm | Up to 12 m or custom cut lengths |
| Welded pipe | OD up to 1219 mm, SCH 10 to SCH 80 and heavier on request | Up to 12 m |
| Welded tube | OD 6–76.2 mm, wall 0.5–6 mm | Continuous or fixed length |
| EP / BA tube | OD 6–50.8 mm, wall 0.5–3 mm | Up to 6–12 m, clean service |
| Coil / U-bend tube | OD 6–25.4 mm, wall 0.5–2 mm | Continuous coil or custom U-bend |
Sizes outside the listed windows are quoted against billet and plate availability. Therefore, state OD, wall, length, condition, and end finish in the inquiry for an accurate route and price.
| Surface Condition | Typical Characteristics / Applications |
|---|---|
| Annealed & Pickled | Standard delivered condition for fabrication and installation |
| Bright Annealed | Smooth, scale-free bore and OD for instrumentation and clean service |
| Pickled Only | Acid-descaled surface for general industrial piping |
| Beveled End | Weld-preparation beveling to the agreed standard for butt welds |
Get detailed information including specifications, standards, dimensions and material properties.
A typical pipe inquiry reaches shipment in two to four weeks, though large-diameter welded product needs longer. Before price is fixed, the sequence below aligns standard, condition, and acceptance with your service plan.
List OD, wall, length, quantity, condition, and the medium and temperature the line carries.
Choose B167 or B163 for seamless routes, and B517 or B516 for welded lines.
Annealed stock suits forming and welding, while as-worked product favors strength.
Price follows the routing, testing scope, documentation, and Incoterm you selected.
The mill runs manufacturing and NDT to the acceptance level agreed at quotation.
Your delivery departs with 3.1 certificates alongside the complete export file.
Feedback from buyers and engineers who source nickel alloy materials from Southerly Alloy.
“The B167 annealed pipe for our caustic evaporator rebuild arrived with hardness records that passed the operator review directly.”
“Dry chlorine line tubing held the specified OD and wall across every shipment, and the certificates matched the heats on delivery.”
“Furnace radiant tube stock was documented heat by heat, so our inspection planning stayed on schedule.”
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B167 covers hot-worked and cold-worked annealed seamless pipe and tube, while B163 covers condenser and heat-exchanger tube. ASME SB167 and SB163 apply under code jurisdiction.
Continuous oxidation service runs to about 1093 °C (2000 °F). Nevertheless, the exact design temperature should be confirmed against pressure and medium for each line.
ERNiCr-3 filler to AWS A5.14 and covered electrodes to A5.11 are the standard choices. Furthermore, most shop and field welds need no preheat.
Yes. Continuous coils and custom U-bends are produced from B163 base material for exchanger fabrication against your bending drawings.
Welded pipe runs from small bore up to OD 1219 mm in schedules from SCH 10 to SCH 80, with heavier walls quoted on request.
One piece is accepted for many stock sizes, so trial lines and repair lengths carry no premium hurdle.
FOB serves as the default Incoterm, while EXW, CIF, and DAP quotes follow confirmed destinations.
Inconel 600 pipe is typically priced by weight (kg) against the ordered size, condition, and required delivery terms. The applicable Incoterm is stated on every quotation.
Mill production for standard sizes runs 7-15 days, and large-diameter welded product is quoted against the confirmed production schedule.
Yes. Every delivery ships with an EN 10204 3.1 certificate, and 3.2 endorsement through a third party is available on request.
Send the OD, wall, length, standard, and quantity, and the reply covers Incoterm, lead time, and documentation. Route and condition questions can ride on the same inquiry for engineering review.