01
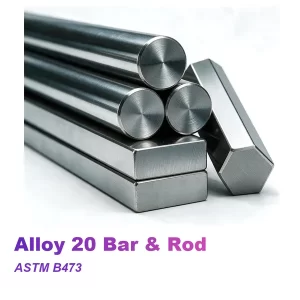
Alloy 20 Cold-Drawn Bright Bar
Drawn stock held inside a commercial h9 to h11 band for bar feeders.
Request Availability →Alloy 20 bright bar held inside commercial h9 to h11 bands so a bar feeder can run unattended.
Copper holds the passive film of this Alloy 20 bright bar alive under reducing conditions, which is what carries it through sulfuric acid.
Moreover, niobium plus tantalum at eight times carbon stabilises this Alloy 20 bright bar, so a weld zone needs no post-weld anneal.
Furthermore, nickel at 32.0–38.0% puts chloride stress corrosion cracking out of reach for this bright bar.
Alloy 20 bright bar comes out of UNS N08020, the niobium-stabilised nickel-iron-chromium grade built around its copper content. Copper between 3.0% and 4.0% and nickel between 32.0% and 38.0% carry this Alloy 20 bright bar through acid duty.
Bright finishing is a route rather than a separate product line, so the B473 floors still govern this grade while the diameter band comes from the drawing. We supply this bright bar to ASTM B473 and ASME SB473 in hot-finished, annealed and cold-finished states, with the ASTM B462 forging route above the bar ceiling and ASTM B472 behind the billets. The heat number, the anneal and quench route we ran and the EN 10204 3.1 report travel with every bright bar consignment.
Meanwhile, the niobium addition is what lets a fabricated vessel of this bright bar go into service without a solution treatment after welding. The full chemistry window and the physical data behind this bright bar sit on our Alloy 20 material page, should you want to cross-reference them.
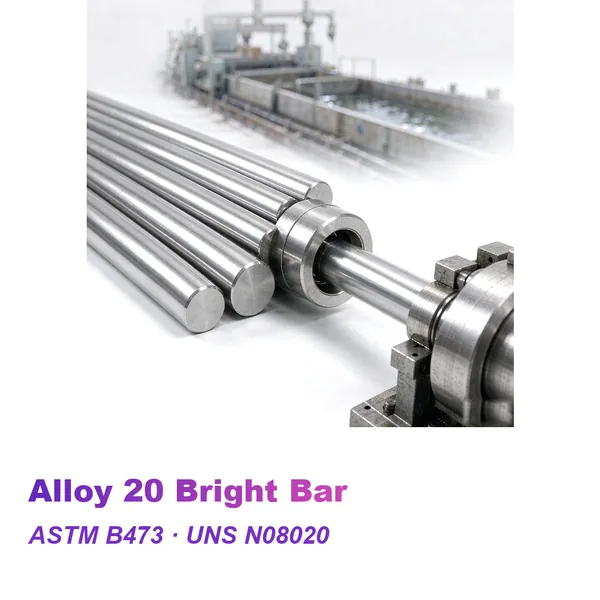
Alloy 20 bright bar comes out of UNS N08020, the niobium-stabilised nickel-iron-chromium grade whose copper content carries it through sulfuric acid. We supply ASTM B473 bright bar cold drawn and polished to commercial h9 to h11 tolerance families for acid plant, pickling house liquor and tankhouse duty. Every Alloy 20 bright bar consignment travels with heat-number traceability, EN 10204 3.1 mill test reports and full export documentation.
For example, 3.0–4.0% copper in this bright bar keeps the passive film alive where a plain austenitic grade loses it.
Specifically, the copper addition lets this bright bar serve across a broad sulfuric acid range rather than only at one end.
Moreover, niobium plus tantalum at eight times carbon keeps the weld zone of this bright bar stable without a furnace pass.
Therefore, nickel above a third of the analysis gives this bright bar immunity to chloride stress corrosion cracking.
In addition, nothing in this bright bar responds to aging, so drawing is the only route above the annealed floor.
Besides, B473 carries no hardness column, so this bright bar clears on chemistry and tensile results alone.
Consequently, NACE MR0175 covers this bright bar at the condition that document names, and we document that condition per heat.
Finally, the austenitic matrix keeps this bright bar non-magnetic for instrument and seal work.
A bright finish earns its premium only when the bar feeds and cuts the way the shop planned. Therefore, we fix the diameter band, the straightness and the roughness of this Alloy 20 bright bar before quoting.
We record the acid, its concentration and its temperature for your Alloy 20 bright bar before proposing a delivery state.
Specifically, each bright bar consignment carries EN 10204 3.1 papers, heat numbers and dimensional records.
In addition, this bright bar flows through one process whether your shop welds it into a vessel or turns it on a lathe.
Quotations for this bright bar name the acid, the section, the finish and the document set rather than leaving them open.
Producing Alloy 20 bright bar runs from charge balancing through to the final pack. We log each stage behind this Alloy 20 bright bar against its own heat number.
We weigh the charge for this bright bar against the B473 analysis and hold carbon at the ceiling.
First, the charge for this bright bar melts and refines under AOD practice that brings carbon down to the ceiling.
Next, we add niobium so that this bright bar carries eight times the carbon content in the finished analysis.
Then, forging and rolling reduce the ingot to this bright bar section between 1230 °C and 925 °C.
After that, we hold this bright bar between 927 °C and 1010 °C so the niobium carbide goes back into solution.
We then drop this bright bar into the tank, because a slow pass through 600–900 °C would precipitate carbide and sigma.
Subsequently, pickling, turning or grinding brings this bright bar to the ordered size and surface.
Finally, we clear this bright bar for dispatch once chemistry, tensile and dimensional checks come back.
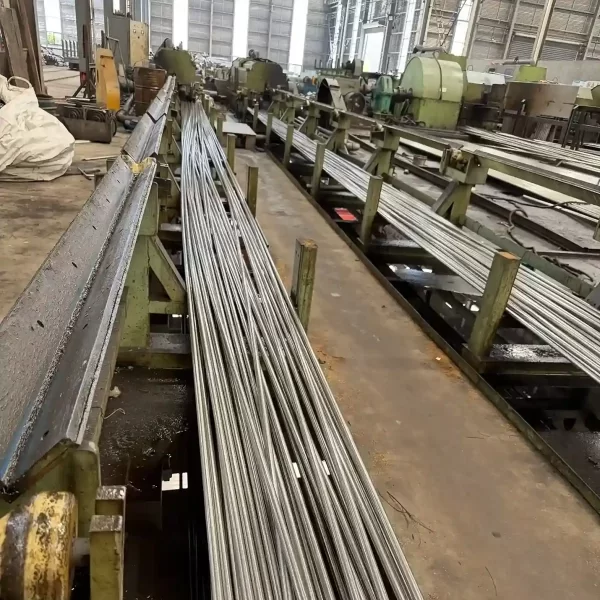
One schedule carries both stock lengths and bespoke heats of Alloy 20 bright bar. Besides, we quote this Alloy 20 bright bar through our bar and rod program.
Hot working, annealing, quenching and finishing lines behind the bright bar share this site.
Units for hot working, annealing, quenching and grinding of this bright bar.
Bright bar tonnage across stock lots and bespoke heats.
Metallurgists who write the anneal and quench plan that this bright bar follows.
In addition, sealed export packing sends this bright bar to buyers on five continents.
Nothing leaves until the heat behind your Alloy 20 bright bar clears our ISO 9001 route. In addition, the checks on this Alloy 20 bright bar follow the requirements the order names.
We match the grade and heat number on this bright bar to your purchase order before anything leaves the yard.
Specifically, copper, nickel and niobium in this bright bar go against the B473 table for your lot.
In addition, every heat of this bright bar carries reported tensile, yield and reduction-of-area values measured against the B473 floor.
The cooling record behind this bright bar travels with its EN 10204 3.1 papers.
The list below covers the variants we quote for Alloy 20 bright bar from your drawing rather than a stock list. In addition, this list covers the deliveries ordered most often for this Alloy 20 bright bar.
Drawn stock held inside a commercial h9 to h11 band for bar feeders.
Request Availability →Ground stock with the diameter band and roundness agreed on the drawing.
Request Availability →Heavy stock peeled first and polished afterwards for a uniform skin.
Request Availability →Stock taken to a stated roughness for sealing and sliding faces.
Request Availability →Diameter, roughness and straightness produced against your drawing.
Request Availability →Alloy 20 bright bar suits plant where sulfuric acid sits in the process rather than visiting it. In addition, the list below sets out where this Alloy 20 bright bar serves.
Discuss Your Application →Bar stock sized for feeders that turn small acid-line fittings around the clock.
Machined holders that keep a flow element square inside an acid line.
Stock turned into wells that stand between a sensor and an acid stream.
Bodies machined from bright stock for impulse lines on corrosive service.
Sleeves turned from bright stock to fit a seal chamber without shimming.
Bushings machined from bright bar for glands that must not drift.
Nipples turned for acid filter housings that open on a schedule.
Bodies machined from bright stock for sample points on a chemical line.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
ASTM B473 prints one chemistry window for this bright bar, holding nickel between 32.0% and 38.0% and copper between 3.0% and 4.0%. Moreover, niobium plus tantalum in this bright bar has to reach eight times the carbon content.
Meanwhile, the full composition table on the Alloy 20 material page carries every limit behind this bright bar.
The floors in the table below come from the B473 bar table for UNS N08020. Therefore, the ordered condition and the ruling section settle final acceptance of Alloy 20 bright bar.
| Condition | Tensile Strength, min. | Yield Strength (0.2%), min. | Elongation, min. | Reduction of Area, min. |
|---|---|---|---|---|
| Stabilised Annealed — UNS N08020 | ≥551 MPa (80 ksi) | ≥241 MPa (35 ksi) | 30% | 50% |
| Strain Hardened, up to 2 in (50.8 mm) | ≥620 MPa (90 ksi) | ≥415 MPa (60 ksi) | 15% | 40% |
Published design data puts the density of this bright bar near 8.08 g/cm³ and its melting range between 1385 °C and 1443 °C. In addition, a modulus close to 193 GPa and a relative permeability near 1.004 leave this bright bar non-magnetic in service.
Therefore, the physical properties table on the Alloy 20 material page holds the conductivity, the resistivity and the expansion figures for this bright bar.
The water quench is the step that defines this Alloy 20 bright bar, because the section has to leave the stabilising anneal fast enough to keep carbide and sigma phases out of the grain boundaries. Moreover, the forging band finishes above 925 °C for a different reason: this grade risks incipient melting near 1200 °C.
| Condition | Typical Treatment |
|---|---|
| Stabilised Annealed | Held between 927 °C and 1010 °C, then water quenched, so the niobium carbide returns to solution |
| Hot-Worked | Forged between 1150 °C and 1230 °C, finishing above 925 °C because the section risks incipient melting near 1200 °C |
| Slow-Cool Caution | Passing slowly through 600–900 °C precipitates carbide and sigma phases, so the quench follows the anneal without delay |
| Strain Hardened | Cold drawn after the anneal, with the strength taken from the reduction rather than from a furnace |
| Cold-Forming Limit | Heavy cold forming sends the section back through the stabilising anneal before it enters service |
| Stress-Relief Caution | A relief pass inside the sensitising band costs corrosion resistance, so the alternative is settled before it is booked |
| Post-Weld Anneal | Most joints enter service as welded, because niobium at eight times the carbon content keeps the weld zone stable |
ASTM B473 is the bar, rod and wire document behind this bright bar, issued by ASTM International. Moreover, ASTM B462 covers forged sections of this bright bar while ASTM B472 governs the billet it is reforged from.
| Standard | Product or Application |
|---|---|
| ASTM B473 / ASME SB473 | Bar, rod and wire, stabilised annealed |
| ASTM B462 / ASME SB462 | Forged bar, forging stock, flanges and fittings |
| NACE MR0175 / ISO 15156-3 | Sour service, at the condition that document sets |
Beyond that, the standards table on the Alloy 20 material page carries the European designations and the flat-product call-outs for this bright bar.
The table below lists the bright bar sizes we ship most often, while the route, the document and the lot size decide what else is possible. Please confirm your own size, section and length with the inquiry.
| Product Form | Typical Supply | Length |
|---|---|---|
| Bright Bar | 3-100 mm dia., cold drawn and polished | Cut to length |
| Cold-Drawn Bright Bar | 3-50 mm dia., h9 to h11 tolerance family | Cut to length |
| Ground Bright Bar | 6-80 mm dia., ground to a close band | Cut to length |
| Peeled and Polished Bar | 20-120 mm dia., turned then polished | Cut to length |
| Polished Bar | To a stated surface roughness | Cut to length |
| Custom Bright Bar | To drawing | Custom |
Bright finishing is a route rather than a separate grade, so the chemistry and the mechanical floors still come from ASTM B473 while the diameter, the straightness and the roughness come from your drawing. Consequently, we agree all three before the bar enters a feeder.
The surface you order on this bright bar decides how the part feeds, seals and resists attack. Consequently, we settle the condition of this bright bar before the price goes out.
| Surface Condition | Typical Use |
|---|---|
| Cold Drawn and Polished | A polished draw pass holds this bright bar in the h8 to h11 band that automatic lathes want. |
| Cold Drawn and Ground | Grinding after drawing tightens the band on this bright bar for bar feeders on a long run. |
| Peeled and Ground | A ground peel route holds this bright bar inside the h9 to h11 band. |
In contrast, the surface finishes table on the Alloy 20 material page lists the further conditions open to this bright bar.
Related forms from the same heat cover Alloy 20 Centreless-Ground Rod, Alloy 20 Forged Bar and Alloy 20 Hex Bar when your bright bar order needs them.
Get detailed information including specifications, standards, dimensions and material properties.
A single coordinator stays with your Alloy 20 bright bar enquiry from the first question to the loading bay. In addition, stock of this Alloy 20 bright bar leaves inside fifteen days, and a freshly annealed heat takes about thirty.
Send the acid, its concentration and its temperature together with the size, quantity and standard this bright bar faces.
Then we lock the anneal cycle, the delivery condition and the tolerance band on this bright bar.
Pricing for this bright bar comes back by size, quantity and destination port.
We need your written confirmation of the specification, the terms and the schedule for this bright bar.
Next we schedule any third-party inspection or dimensional review of this bright bar before production starts.
This bright bar reaches you with mill papers, a packing list and the certificate set.
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B473 and ASME SB473 cover this Alloy 20 bright bar, with the ASTM B462 forging route taking over above the bar ceiling.
No. B473 prints tensile, yield, elongation and reduction of area with no hardness column, so we release this bright bar on those four figures.
Yes. NACE MR0175 covers this grade, and the condition it sets for your bright bar is what we document per heat.
ER320LR bare wire to AWS A5.9 joins this bright bar, with E320LR covered electrodes to AWS A5.4 for manual work.
A slow pass through 600–900 °C precipitates carbide and sigma at the grain boundaries, so each bright bar heat leaves the anneal straight into the tank.
Usually not. Niobium at eight times the carbon content stabilises the matrix, so most bright bar joints stay serviceable as welded.
Trial lengths of this bright bar are welcome, and one piece covers most stock sizes.
Trade terms for this bright bar open on FOB, and EXW, CIF or DAP follow once we know the destination port.
Stock sizes of this bright bar ship in 7 to 15 days, while a made-to-order annealed heat needs about 30 days.
EN 10204 3.1 papers cover every heat of this bright bar, and we can arrange a 3.2 endorsement.
Our Alloy 20 bright bar offer fixes the diameter band, the straightness and the roughness before the price. Send those three figures with your quantity to receive pricing for this Alloy 20 bright bar.
Your bright bar inquiry passes through the anneal, the finish and the document scope before any price goes out. We build to the signed sheet, and the full paper set travels with this bright bar.