01
Hastelloy B-3 ERNiMo-10 Bare Wire
AWS A5.14 solid nickel-molybdenum filler for GTAW, GMAW and plasma work.
Request Availability →ERNiMo-10 bare wire and ENiMo-10 electrodes for joining Hastelloy B-3 vessels and dissimilar steel.
ERNiMo-10 covers the bare form of this Hastelloy B-3 welding wire, while ENiMo-10 covers the covered electrode.
Moreover, the nickel-molybdenum deposit from this Hastelloy B-3 welding wire keeps the reducing-acid behaviour of the original fabrication.
Furthermore, this Hastelloy B-3 welding wire leaves in sealed tubes, spools and electrode packs sized for a turnaround window.
Hastelloy B-3 welding wire covers the fillers classified for joining UNS N10675 fabrications. The bare form of this Hastelloy B-3 welding wire runs as ERNiMo-10 per AWS A5.14. Its covered electrode runs as ENiMo-10 per AWS A5.11.
We supply Hastelloy B-3 welding wire as straight TIG rods, wound MIG spools and sealed electrode packs. The deposit carries the reducing-acid performance of the parent metal through the joint, and the slower precipitation of this grade means a finished weld usually needs no further furnace pass.
Meanwhile, the base-metal chemistry behind this Hastelloy B-3 welding wire sits on our Hastelloy B-3 material page for weld procedure work.
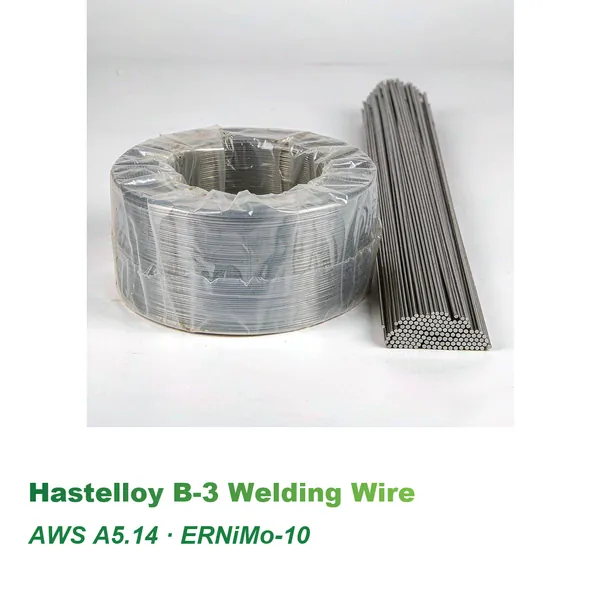
Hastelloy B-3 welding wire arrives in UNS N10675, the nickel-molybdenum grade that carries 1.0–3.0% chromium on purpose, which slows the embrittling phase enough that most welded joints enter service without a furnace pass. We supply ASTM B335 welding wire as ERNiMo-10 bare wire, TIG lengths and MIG spools for hydrogen chloride synthesis, acid regeneration and steel pickling hardware. Every Hastelloy B-3 welding wire consignment travels with heat-number traceability, EN 10204 3.1 mill test reports and full export documentation.
For example, an ERNiMo-10 deposit from this Hastelloy B-3 welding wire carries the parent metal's reducing-acid performance into the joint.
Specifically, the ENiMo-10 electrode of this Hastelloy B-3 welding wire covers manual repair work in awkward positions.
Moreover, AWS A5.14 covers the bare wire used as this Hastelloy B-3 welding wire while A5.11 covers the covered electrode.
In addition, the slower Ni3Mo kinetics of this grade let a finished weld in this Hastelloy B-3 welding wire stay as welded.
Besides, a gas-tungsten deposit from this Hastelloy B-3 welding wire holds room-temperature impact energy near 224 J.
Every pack of this Hastelloy B-3 welding wire ships sealed against moisture so the surface arrives weld-ready.
Documentation for this Hastelloy B-3 welding wire follows EN 10204 3.1 from spool to spool.
Therefore, we can pack this Hastelloy B-3 welding wire to the quantity a single shutdown actually needs.
The deposit has to hold the reducing-acid performance of the parent metal through a repair, so the class decides everything. In addition, we confirm the AWS class, diameter and pack weight of this Hastelloy B-3 welding wire before quoting.
We record the medium, its concentration and its temperature for your Hastelloy B-3 welding wire before proposing a delivery state.
Specifically, EN 10204 3.1 papers, heat numbers and dimensional records follow each Hastelloy B-3 welding wire consignment.
In addition, this Hastelloy B-3 welding wire flows through a single process whether your shop welds it into a vessel or turns it on a lathe.
Quotations for this Hastelloy B-3 welding wire name the medium, the section, the finish and the document set rather than leaving them open.
We balance melt stock for this filler to the nickel-molybdenum window before anything else happens. From there, we log every step behind this Hastelloy B-3 welding wire against a heat number.
We weigh nickel, molybdenum and a controlled chromium addition, then balance the analysis this Hastelloy B-3 welding wire needs.
First, the charge for this Hastelloy B-3 welding wire melts and casts into electrode stock under a tight carbon ceiling.
Next, rolling and drawing bring this Hastelloy B-3 welding wire down to the ordered filler diameter.
Then, pickling and mechanical cleaning leave this Hastelloy B-3 welding wire bright and ready for the arc.
After that, we wind spools and cut straight TIG lengths of this Hastelloy B-3 welding wire.
For ENiMo-10, we press the covering onto this Hastelloy B-3 welding wire core wire.
Subsequently, we bake and seal covered electrodes of this Hastelloy B-3 welding wire against moisture pickup.
Finally, all-weld-metal checks confirm the class of this Hastelloy B-3 welding wire before we issue the certificate.
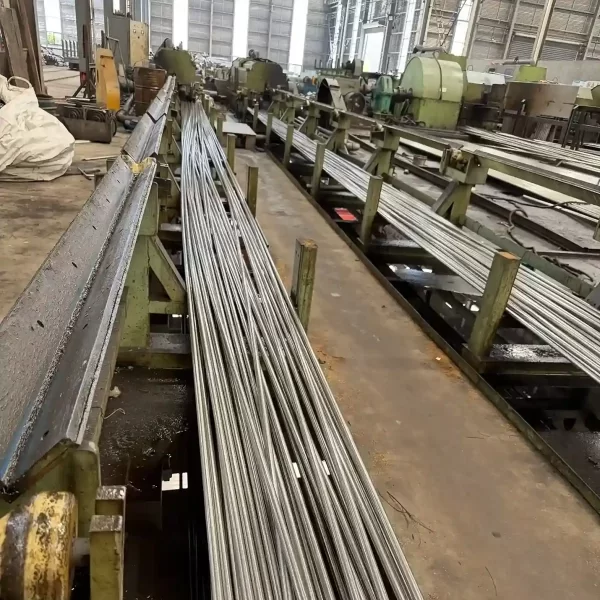
Stock lengths and made-to-order heats of Hastelloy B-3 welding wire leave on one production schedule. Moreover, we quote this Hastelloy B-3 welding wire inside our bar and rod program.
Hot working, annealing, drawing and pickling lines for Hastelloy B-3 welding wire share one site.
Units covering hot working, annealing, drawing and pickling for this Hastelloy B-3 welding wire.
Hastelloy B-3 welding wire output across stock and bespoke lots.
Metallurgists who set the anneal plan and the delivery state of this Hastelloy B-3 welding wire against your duty.
In addition, sealed export packing carries this Hastelloy B-3 welding wire to buyers on five continents.
Nothing leaves the yard until the heat behind your Hastelloy B-3 welding wire has cleared our ISO 9001 inspection route. In addition, we test this Hastelloy B-3 welding wire against the chemistry, tensile and surface the order names.
We confirm the grade and heat number of this Hastelloy B-3 welding wire against your purchase order.
Specifically, molybdenum, chromium and carbon in this Hastelloy B-3 welding wire go against the B335 table for your lot.
In addition, we report the tensile and yield results of this Hastelloy B-3 welding wire against the B335 minimums for every heat.
Every consignment of this Hastelloy B-3 welding wire ships with EN 10204 3.1 papers keyed to its heat.
We quote sections and delivery states for Hastelloy B-3 welding wire against the drawing rather than from a catalogue. In addition, the list below shows the Hastelloy B-3 welding wire forms ordered most often.
AWS A5.14 solid nickel-molybdenum filler for GTAW, GMAW and plasma work.
Request Availability →Straight ERNiMo-10 lengths cut at 914 mm in sealed tubes.
Request Availability →ERNiMo-10 wire wound on spools for semi-automatic GMAW.
Request Availability →AWS A5.11 covered electrodes with a matching core for repair work.
Request Availability →Filler wound against your spool size, weight and length schedule.
Request Availability →Filler for this grade earns its place where a repair has to restore the corrosion performance of the original fabrication. Therefore, the list below shows the duties this Hastelloy B-3 welding wire covers.
Discuss Your Application →Filler for shells, heads and internals across UNS N10675 fabrications.
Welding internals that face acid inside hydrogen chloride absorption columns.
Joints between this grade and austenitic stainless steel components.
Nickel filler joints to carbon steel where a lining stops.
Deposits laid on steel shells to give a reducing-acid contact surface.
Filler for weld repair on plant already built in this grade.
Welding vessels and pipework inside waste acid regeneration units.
Deposits used to clad and rebuild acid-exposed surfaces.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
Chromium sits deliberately between 1.0 and 3.0% in this welding wire, and that addition is what separates the UNS N10675 window from the earlier nickel-molybdenum grades. Consequently, molybdenum holds 27.0–32.0% while carbon stops at 0.01%, so the nickel-plus-molybdenum total of this welding wire lands between 94.0 and 98.0%.
For every element measured against its B335 limit behind this welding wire, open the composition breakdown kept on the Hastelloy B-3 material page.
All-weld-metal results for the fillers supplied with Hastelloy B-3 welding wire appear below, taken from published weld test data. Note that the bare wire classification carries no tensile floor from AWS, so chemistry and the test report carry the release.
| Product (all-weld metal) | AWS Class | Tensile Strength | Elongation |
|---|---|---|---|
| ERNiMo-10 bare wire, GTAW deposit | AWS A5.14, UNS N10675 | 813 MPa (118 ksi), typical | 45%, typical |
| ERNiMo-10 bare wire, GMAW deposit | AWS A5.14, UNS N10675 | 834 MPa (121 ksi), typical | 46%, typical |
| ENiMo-10 covered electrode, SMAW deposit | AWS A5.11, UNS W80675 | 772 MPa (112 ksi), typical | 49%, typical |
Identification data for the parent metal and for both deliveries appears below for this Hastelloy B-3 welding wire.
| Property | Value |
|---|---|
| Parent Metal | UNS N10675, 2.4600 / NiMo29 |
| Bare Filler | ERNiMo-10 (AWS A5.14) |
| Covered Electrode | ENiMo-10 (AWS A5.11) |
| Covered Electrode UNS | W80675 |
| Molybdenum | 27.0–32.0% in the parent metal |
| Chromium | 1.0–3.0% deliberately added to the parent metal |
| Carbon | 0.01% max. in the parent metal |
| Nickel plus Molybdenum | 94.0–98.0% combined in the parent metal |
| Strengthening Route | Cold work only, because the grade takes nothing from aging |
Specifically, the classification data below sets out the deposit side of this Hastelloy B-3 welding wire in both of its packaged forms.
| Product | AWS Class | Chemistry Basis | Typical Strength | Best Suited For |
|---|---|---|---|---|
| Bare wire | ERNiMo-10 (A5.14), UNS N10675 | Ni balance, Mo 27.0–32.0%, Cr 1.0–3.0%, Fe 3.0% max., C 0.02% max. | 813–834 MPa (118–121 ksi) typical | GTAW primary, GMAW general |
| Covered electrode | ENiMo-10 (A5.11), UNS W80675 | The same nickel-molybdenum analysis under a basic covering | 772 MPa (112 ksi) typical | SMAW repair and build-up |
The bare filler for this welding wire runs as ERNiMo-10 under AWS A5.14, a classification issued by the American Welding Society. Moreover, AWS A5.11 covers the ENiMo-10 electrode that pairs with this welding wire. Besides, ASME SFA-5.14 mirrors the bare filler document for pressure work.
| Standard | Product or Application |
|---|---|
| AWS A5.14 | ERNiMo-10 bare nickel-molybdenum welding wire |
| AWS A5.11 | ENiMo-10 covered electrode, UNS W80675 |
| ASME SFA-5.14 | ASME version of the bare filler specification |
Finally, the full standards list on the Hastelloy B-3 material page adds the plate, tube, fitting and flange documents plus the Chinese designation behind this welding wire.
Dimensions of Hastelloy B-3 welding wire follow the route, the document and the order quantity. Therefore, typical supply ranges sit in the table below, so please confirm your sizes in the inquiry.
| Product Form | Typical Supply | Length |
|---|---|---|
| TIG Filler Rod (GTAW) | 1.6 / 2.4 / 3.2 mm × 914 mm | 5 kg tube |
| MIG Wire (GMAW) | 0.9 / 1.2 / 1.6 mm | Spool |
| Coiled Wire | 0.9 / 1.1 / 1.6 mm dia. | Coil |
| Straight Cut Lengths | 1.6–3.2 mm dia. | Straight lengths |
| Covered Electrode (SMAW) | 2.4 / 3.2 / 4.0 mm | Sealed pack |
| Custom Winding | To drawing | Custom |
Available sizes of this Hastelloy B-3 welding wire depend on the route, the document, the state and the lot size. Please confirm the size, section and length you need for this welding wire in the inquiry.
Bare filler of this grade is classified as ERNiMo-10 under AWS A5.14 with UNS N10675, and the covered electrode as ENiMo-10 under AWS A5.11 with UNS W80675. Moreover, ASME SFA-5.14 mirrors the bare document, and the standard product forms run from 0.76 to 4.70 mm with straight TIG lengths cut at 914 mm.
The surface you order decides how this welding wire behaves once it reaches a hydrogen chloride synthesis unit, an absorption tower or an acid regeneration loop. Moreover, most stock of this welding wire leaves the yard solution annealed and pickled. Therefore, we confirm the finish and the straightness band on this Hastelloy B-3 welding wire before we write the offer.
| Surface Condition | Typical Use |
|---|---|
| Clean Bright | The standard surface for bare ERNiMo-10 welding wire, free of drawing lubricant. |
| Straight Rods | Cut TIG lengths of this welding wire with clean, deburred ends. |
| Spooled | This welding wire wound onto spools or carriers at an even tension. |
In addition, the surface finishes table recorded on the Hastelloy B-3 material page lists the remaining conditions quoted for this welding wire.
Related forms from the same heat cover Hastelloy B-3 Wire, Hastelloy B-3 Bright Bar and Hastelloy B-3 Centreless-Ground Rod when your welding wire order needs them.
Get detailed information including specifications, standards, dimensions and material properties.
One coordinator stays with your Hastelloy B-3 welding wire enquiry from the first question through to loading. Therefore, stock sizes of this Hastelloy B-3 welding wire dispatch inside fifteen days, while a fresh annealed heat runs about twenty-five.
Give us the medium, its concentration and its temperature, plus the size, quantity and standard this Hastelloy B-3 welding wire will face.
Then we set the annealing cycle, the delivery state and the tolerance band for this Hastelloy B-3 welding wire.
Pricing for this Hastelloy B-3 welding wire arrives by size, quantity and destination port.
You confirm the specification, the terms and the schedule of this Hastelloy B-3 welding wire in writing.
We book any third-party inspection or dimensional review of this Hastelloy B-3 welding wire before production starts.
This Hastelloy B-3 welding wire arrives with mill papers, a packing list and the certificate set.
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ERNiMo-10 per AWS A5.14 covers the bare form of this Hastelloy B-3 welding wire, and ENiMo-10 per AWS A5.11 covers the covered electrode.
No. The A5.14 nickel-molybdenum classes are classified on chemistry rather than strength, so we report all-weld-metal values from the test certificate.
Usually not. Because Ni3Mo forms slowly near 650 °C, most welds made with this Hastelloy B-3 %s stay in the as-welded condition, unlike the older B grade.
GTAW, GMAW, PAW and SMAW all work with this Hastelloy B-3 welding wire, while submerged arc stays out because the flux disturbs the deposit chemistry.
Ferric ions, cupric ions, nitric acid and hypochlorite, so filler work on this Hastelloy B-3 welding wire has to confirm an oxidant-free stream.
Weight in kilograms drives pricing for this Hastelloy B-3 welding wire, with the prevailing nickel and molybdenum quotations applied on the order date.
A single sealed tube or spool covers many common diameters of this Hastelloy B-3 welding wire.
We quote FOB as standard for this Hastelloy B-3 welding wire, and EXW, CIF or DAP terms follow once we fix the destination.
Expect 7 to 15 days on stock sizes of this Hastelloy B-3 welding wire, and custom packing takes longer.
Every batch of this Hastelloy B-3 welding wire ships with EN 10204 3.1, and we book a 3.2 endorsement through the order.
We quote Hastelloy B-3 welding wire by AWS class, diameter and pack weight. Send the classification, diameter and quantity you need to price this Hastelloy B-3 welding wire.
We walk your Hastelloy B-3 welding wire inquiry through the anneal, the finish and the document scope, then quote on clear terms. Production then follows the signed sheet, and every consignment of this Hastelloy B-3 welding wire leaves with the complete paper set.