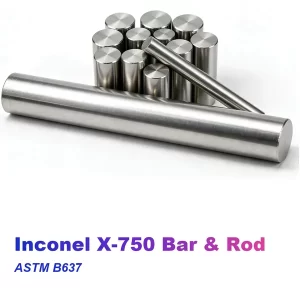
01
Peeled Bright Bar
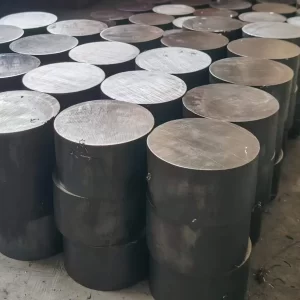
Peeled rounds from 20 to 300 mm carry a machined skin for further turning.
Request Availability →Cold-finished bright stock in three cycles for close-tolerance machined parts and turned components.
A single Inconel X-750 bright bar reaches 965, 1103 or 1170 MPa minimum tensile once the mill fixes the cycle.
Every bright bar leaves our line turned, peeled or drawn, so no scale reaches your machine.
We hold X-750 bright bar diameter to h9 or h11, whichever your part calls for.
Inconel X-750 bright bar ships in UNS N07750, a precipitation-hardening nickel-chromium-iron alloy. Titanium and aluminium build the gamma-prime precipitate inside this cold-finished stock. Niobium then slows its coarsening, so the bright bar holds strength to 704 °C.
We supply Inconel X-750 bright bar to ASTM B637 in the Type 1, Type 2 and Type 3 conditions. Consequently, the ordered cycle decides the strength level of the bright bar, and we record it on the purchase order before production.
Meanwhile, the Inconel X-750 Bar and Rod hub also lists this bright bar beside the other forms. The European call-out NiCr15Fe7TiAl maps to the same UNS N07750 material as this bright bar.
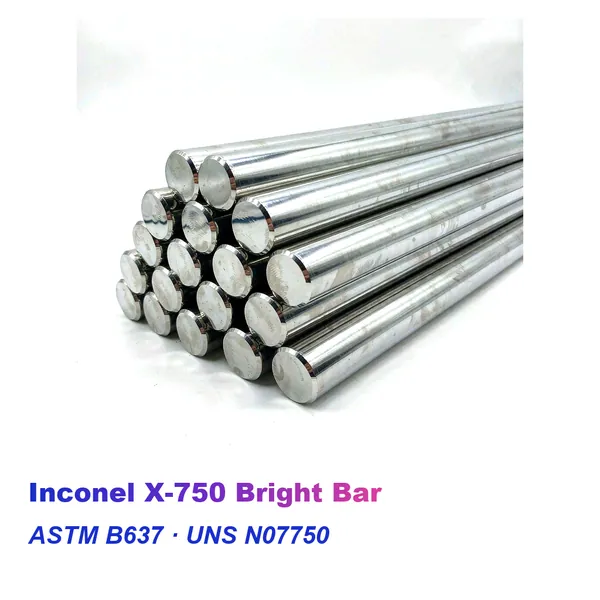
Inconel X-750 bright bar is supplied in UNS N07750, the precipitation-hardening nickel-chromium-iron alloy strengthened by gamma prime. Titanium, aluminium and niobium build the precipitate that holds strength to 704 °C. Southerly Alloy supplies and exports X-750 bright bar to ASTM B637 in the Type 1, Type 2 and Type 3 conditions, with EN 10204 3.1 paperwork on every heat.
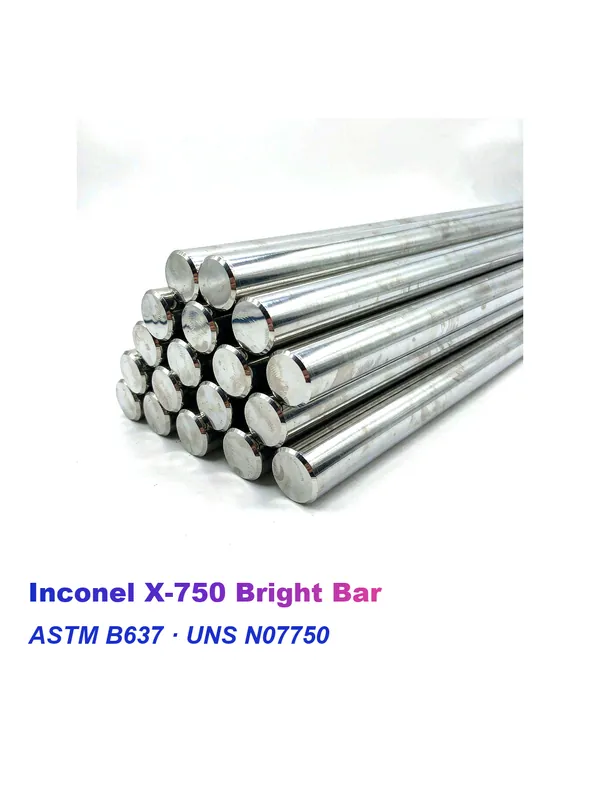
Type 2, Type 3 and Type 1 deliver 1170, 1103 and 965 MPa minimum tensile for Inconel X-750 bright bar in that order.
Specifically, bright bar holds a closer diameter band than hot-finished stock of the same size.
Moreover, the stabilised Type 1 route guards the creep strength of bright bar where the part runs hot for years.
Therefore, bright bar goes straight into the machine without pickling or rough turning.
Each bright bar lot travels with the furnace chart for its own solution treatment and age.
The hardened bright bar matrix machines with carbide tooling rather than heavy cuts.
We check bright bar straightness so the bar feeds a bar feeder without whip.
In fact, we ship bright bar in coils or in cut straight lengths.
Sourcing Inconel X-750 bright bar depends on agreeing the finish and the cycle together. Where a bar feeder runs the stock, the straightness and the diameter band decide the yield.
Grade, bright diameter, finish and cycle enter the purchase order at the same time.
Consequently, each certificate records the solution and aging that the mill applied to that bright bar heat.
In addition, we state the bright bar diameter band and the surface condition on the offer.
Quotations for Inconel X-750 bright bar include the packing list, mill certificate and export documents.
One melt feeds every bright bar section, and the ordered cycle then sets the final properties. Because titanium and aluminium oxidise easily, melting control for X-750 bright bar matters as much as the finishing pass.
Weighed nickel, chromium, iron, titanium and aluminium enter the melt that will become this bright bar order.
Vacuum induction melting holds titanium and aluminium inside a narrow window on every bright bar heat.
Consumable electrode or vacuum arc remelting follows, and the certificate records the route taken for the bright bar.
Forging and rolling reduce the ingot to bright bar stock above the recrystallisation temperature.
Turning, peeling or drawing then brings the bright bar to its ordered diameter and surface.
The bright bar holds at 982, 1093 or 1149 °C, as the ordered Type requires.
Consequently, the Type 1 route adds a hold near 843 °C, and every bright bar then ages near 704 °C.
Finally, we gauge the bright bar diameter, straightness and surface before the lot is released.
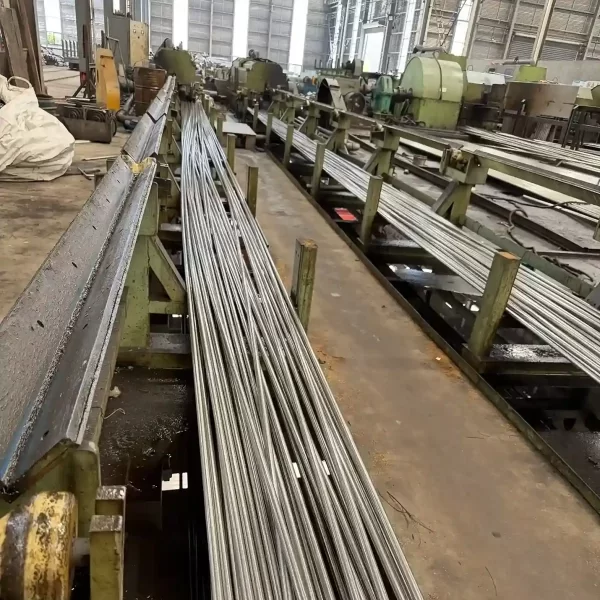
Southerly Alloy supplies Inconel X-750 bright bar across the common cold-finished diameters and conditions. We confirm bright bar diameter, tolerance and finish against your order before production.
Melting, forging, heat treatment and finishing for Inconel X-750 bright bar sit inside one boundary.
Peelers, draw benches, grinders and polishers cover the bright bar sizes we stock.
Custom bright bar heats and stocked diameters share one campaign calendar.
A metallurgist reviews every X-750 bright bar enquiry before the offer leaves.
Chemistry and heat treatment decide these bright bar properties together, so our laboratory checks both. Therefore, the certificate reports the cycle that produced the bright bar values.
The laboratory reads titanium, aluminium and niobium in the bright bar heat, then records each figure against the ASTM table.
Specifically, tensile and yield values for this bright bar come from aged stock rather than solution-treated material.
In addition, we gauge bright bar diameter, ovality and straightness against the agreed tolerance.
Consequently, every bright bar certificate carries the solution and aging record for the same heat.
Different bright bar finishes suit different machining setups. Therefore, the list below shows the Inconel X-750 Bright Bar variants we quote most often.
Peeled rounds from 20 to 300 mm carry a machined skin for further turning.
Request Availability →Ground stock held to h9 diameter for shafts and pins.
Request Availability →Drawn bright bar with the scale removed and a smoother surface.
Request Availability →Bright bar delivered in the Type 2 or Type 3 condition for immediate service.
Request Availability →Custom Inconel X-750 bright bar produced against your own specification.
Request Availability →Hot valve work and close-tolerance shafting are where Inconel X-750 bright bar has served longest. Meanwhile, the Instrument trade relies on this cold-finished stock wherever a part must hold size.
Discuss Your Application →Stems turned from X-750 bright bar for high-temperature valves.
Shafts machined from bright bar that run true at temperature.
Bright bar fittings for hot gas sampling lines.
Housings machined from bright bar for furnace sensors.
Stud blanks cut from bright bar for hot bolting.
Pins machined from bright bar for hot assemblies.
Bright bar stock for gauges that hold size in service.
Bright bar parts machined for in-vessel hardware.
Detailed technical information including chemical composition, mechanical properties, standards and available dimensions.
The limits come from ASTM B637, which shares one composition table with the AMS documents for UNS N07750. Titanium and aluminium set the gamma-prime volume in this bright bar, while niobium slows its coarsening.
Iron balances the matrix, and the nickel plus cobalt floor keeps this bright bar austenitic. The full composition table on the Inconel X-750 material page lists every element against its ASTM limit.
The three bar rows reproduce ASTM B637 Table 3 for UNS N07750. Section size matters for Type 2, because heavy bar relaxes to a lower elongation floor. Every value below is a minimum unless the row states a range.
| Product Form | Condition | Tensile Strength, min. | Yield Strength (0.2%), min. | Elongation, min. | Hardness |
|---|---|---|---|---|---|
| Bar and rod, ASTM B637 Type 2 | Solution treated at 982 °C, aged | >=170 ksi (1170 MPa) | >=115 ksi (790 MPa) | 18% | 302-363 HB |
| Bar and rod, ASTM B637 Type 3 | Solution treated at 1093 °C, aged | >=160 ksi (1103 MPa) | >=100 ksi (689 MPa) | 20% | 267-363 HB |
| Bar and rod, ASTM B637 Type 1 | Solution treated at 1149 °C, stabilised, aged | >=140 ksi (965 MPa) | >=90 ksi (620 MPa) | 8% | 262 HB min. |
Type 2 holds over sections up to 63.5 mm, and heavier bar relaxes to 15% elongation and 15% reduction of area. Type 1 trades tensile strength for creep life above 593 °C, which explains its lower elongation floor. Hardness ranges are informative only.
Design work leans on the published figures for this grade, and density sits at 8.28 g/cm³. Moreover, the magnetic behaviour of this bright bar changes with the heat treatment applied, so the Curie temperature follows the cycle.
The physical properties table on the Inconel X-750 material page carries the remaining values, including the modulus and the thermal expansion.
Inconel X-750 is precipitation hardened, so the cycle rather than a simple anneal sets its final strength. We supply the stock in the condition below that your duty needs.
| Condition | Typical Treatment |
|---|---|
| Type 2 (single age) | Solution treated at 982 °C, then aged near 704 °C |
| Type 3 (single age) | Solution treated at 1093 °C, then aged near 704 °C |
| Type 1 (stabilised) | Solution treated at 1149 °C, stabilised near 843 °C, then aged |
| Solution treated only | Soft stock for buyers who machine and age afterwards |
ASTM B637 is the principal UNS N07750 bar specification, and the AMS 5667 group covers the same forms by melting route. The three designations below settle most enquiries.
| Standard | Product or Application |
|---|---|
| ASTM B637 / ASME SB637 | Bars, forgings, and forging stock for moderate or high temperature service |
| AMS 5667 | Bars, forgings, and rings, equalized and precipitation hardenable |
| UNS N07750 - W.Nr. 2.4669 - NiCr15Fe7TiAl | Material designations |
The full standards list on the Inconel X-750 material page adds the AMS 5668 group, the NACE sour service qualification and the Chinese and Japanese designations.
Pyromet X750, Nickelvac X750, Nicrofer 7016 TiNb, and Inconel are trademarks of their respective owners. We quote those names for reference only, and our deliveries follow the ASTM and AMS documents listed above.
The standard text from ASTM International settles any acceptance question.
Because ASTM B637 prints its own scope, the bright bar ranges below follow that text rather than one house rule. For that reason, state the bright bar diameter, the tolerance and the ordered length on the enquiry.
| Product Form | Typical Supply Range |
|---|---|
| Bright bar | 3-100 mm diameter, cold finished to ASTM B637 |
| Peeled bright bar | 20-300 mm diameter with a machined skin |
| Ground bright bar | 3-100 mm diameter held to h9 |
| Bright bar, close tolerance | Tight diameter and straightness by agreement |
Cut lengths of this bright bar run from 1 m up to 6 m as standard, and the AMS bar documents cap their scope at 254 mm. Therefore, heavier sections ship as forged product against the same standard.
Finish follows the operation that comes next rather than a catalogue default. Moreover, we agree the surface of this bright bar with your order.
| Surface Condition | Typical Use |
|---|---|
| Cold drawn | Close size control and a brighter surface on this bright bar. |
| Peeled | A machined skin gives this bright bar uniform diameter for further turning. |
| Bright annealed | A scale-free surface on this bright bar for instrument and clean circuits. |
Any neighbouring section ships from the same heat, including cold drawn bar, polished bar and centreless ground rod.
Get detailed information including specifications, standards, dimensions and material properties.
Eight steps carry a bright bar enquiry from the first message to the delivered lot. Therefore, state the bright bar duty first, and the cycle then follows from it.
Give the service temperature, the load and the medium that the bright bar part will meet.
Tell us that the order is X-750 bright bar rather than hot-finished bar or wire.
We agree Type 1, Type 2 or Type 3 for the bright bar against that duty.
The quotation states the bright bar price per kilogram, the lead time and the certificate set.
Grade, bright bar diameter, tolerance and inspection level enter the order acknowledgement.
The melt shop weighs the charge and takes the bright bar heat through melting and remelting.
The bright bar passes the ordered cold finishing, the heat treatment and release testing.
Finally, the desk tracks the bright bar shipment and forwards the documents ahead of arrival.
Our production and inspection processes are certified to international standards, and every delivery ships with EN 10204 3.1 mill test certificates.
Quality Management System
Pressure Equipment Directive
Material Standards Compliance
Mill Test Certificates
ASTM B637 governs the bar, forging and ring forms of UNS N07750. In addition, the AMS 5667 group covers the same forms by melting route and solution treatment.
Type 2 suits bright bar below about 593 °C, because it carries the highest tensile floor at 1170 MPa. Above that temperature, the stabilised Type 1 cycle is the better choice.
Bright bar runs from 3 to 100 mm diameter cold finished, while peeled bright bar reaches 300 mm with a machined skin.
Bright bar holds h9 or h11 bands under ISO 286-2 as standard. In addition, we quote tighter bands where the bar feeder needs them.
It adds a stabilising hold near 843 °C after the solution treatment of the bright bar. Consequently, the Type 1 route protects creep life above 593 °C at some cost in tensile strength.
Yes. The AMS bar documents cover solution-treated and equalized conditions for buyers who machine the bright bar parts first and age them afterwards.
A single piece or one coil covers most stock sizes of bright bar, so a short cut is enough for a trial.
We quote bright bar mainly on FOB terms, and EXW or CIF follow on request.
Stock bright bar ships in 7 to 15 days, and made-to-order material runs about 25 days.
Yes. Every heat ships with an EN 10204 3.1 certificate, and we arrange 3.2 endorsement on request.
Send the bright bar diameter, the tolerance and the service temperature. The quotation carries the bright bar price, the lead time and the certificate set. Because the cycle decides the acceptance level for this bright bar, name the Type at enquiry.
A single X-750 bright bar proves the grade before a plant-wide commitment.