The Hardness of Nickel Alloys
A technical overview of hardness measurement systems, conversion methods, and how nickel-based alloys behave under different heat treatment and service conditions.
1. Introduction to Nickel Alloy Hardness
Nickel alloys are widely used in aerospace, chemical processing, marine engineering, and energy industries due to their excellent corrosion resistance and high-temperature stability. One of the key mechanical properties used to evaluate these materials is hardness.
Hardness reflects a material’s resistance to indentation, wear, and plastic deformation. For nickel-based superalloys, hardness is closely related to heat treatment condition, especially aging and solution strengthening processes.
Because different industries use different testing systems, hardness comparison often requires standardized conversion references.
2. Common Hardness Testing Methods for Nickel Alloys
Brinell Hardness (HB)
Brinell hardness uses a carbide or steel ball indenter under a fixed load. It is commonly applied to castings and forged nickel alloy blocks where surface area is relatively large.
Rockwell Hardness (HR)
Rockwell hardness, especially HRC, is widely used in nickel alloys such as Inconel 718, Inconel 625, and Inconel 901. It measures indentation depth and is suitable for heat-treated components.
Vickers Hardness (HV)
Vickers hardness uses a diamond pyramid indenter and is suitable for precision measurement of thin sections and high-strength nickel alloys.
3. Hardness Behavior of Nickel-Based Superalloys
Unlike carbon steels, nickel alloys do not rely on simple phase transformation hardening. Instead, their hardness is mainly controlled by:
- Precipitation strengthening (e.g., gamma prime phase)
- Solid solution strengthening
- Heat treatment conditions (solution + aging)
For example, alloys such as Inconel 718 or Inconel 901 can significantly increase hardness after aging treatment, even if the initial forged state shows moderate hardness values.
4. Nickel Alloy Hardness Conversion Table (Engineering Reference)
The following table provides a practical reference for converting hardness values commonly used in nickel alloy engineering. These values are approximate and used in industrial quality control.
| Brinell Hardness (HB) | Rockwell C (HRC) | Vickers Hardness (HV) |
|---|---|---|
| 120 | ~10 | 125 |
| 150 | ~15 | 160 |
| 200 | ~20 | 210 |
| 250 | ~25 | 260 |
| 300 | ~30 | 310 |
| 350 | ~35 | 360 |
| 400 | ~40 | 410 |
| 450 | ~45 | 460 |
5. Factors Affecting Hardness in Nickel Alloys
Hardness variation in nickel-based alloys is influenced by several key factors:
- Heat treatment process (solution annealing and aging)
- Alloy grade (e.g., Inconel 625 vs Inconel 718 vs Inconel 901)
- Grain size and microstructure
- Chemical composition and impurity control
For instance, precipitation-hardened alloys such as Inconel 718 show a significant hardness increase after aging, while solid-solution alloys like Inconel 625 remain relatively stable.
6. Engineering Applications of Hardness Data
Hardness testing plays a critical role in quality control and engineering validation of nickel alloys.
- Heat-treated aerospace components
- Chemical processing equipment
- Gas turbine and energy systems
- Corrosion-resistant piping and fittings
In production environments, hardness is often used as a fast inspection method to verify whether heat treatment has achieved the required mechanical properties.
7. Case Study: Meeting a 38 HRC Requirement on Inconel 901
Hardness specification is where the theory above meets a purchase order. The following case comes from a production enquiry for Inconel 901 plate that asked for a hardness well above the grade’s normal band. It shows how much of the final result depends on process control rather than on chemistry.
7.1 The requirement
An overseas customer required Inconel 901 plate at a target hardness of 38 HRC. Standard material data puts the typical hardness range of Inconel 901 at roughly 30–35 HRC, so the requirement sat clearly above the normal specification and turned into a heat-treatment control problem rather than a purchasing one.
Engineering review concluded that an optimised forging route followed by controlled ageing could reach the target, and the order was accepted on that basis.
7.2 Raw material and forging strategy
The order was small, but material control stayed critical because the final cutting dimensions had to be guaranteed. The customer needed roughly 25 kg of finished material; to keep machining stable after forging and heat treatment, the forging block was increased to 35 kg.
Raw material was specified as pre-forged stock taken through multiple forging cycles, which evens out the structure and stabilises the mechanical response in later stages. That requirement extended the procurement cycle and pushed the original delivery date out.
The forging route itself involved repeated heating, forging, and annealing cycles. Because the batch was small it had to be run alongside other production lots, which stretched the schedule further. The forged block arrived after about three weeks at an actual weight of 38.3 kg.
7.3 Incoming inspection and heat treatment
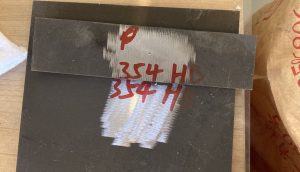
On receipt, the block went through spectral analysis and hardness testing. Chemical composition met specification, with sulfur slightly elevated but inside the acceptable limit. Initial hardness readings were:
- 32 HRC
- 32 HRC
- 34 HRC
That confirmed a real gap against the 38 HRC target. Solution treatment followed by a controlled ageing cycle was then used to raise precipitation strengthening in the matrix. The ageing step holds the material in a defined temperature window long enough for the strengthening phases to form, which lifts hardness, wear resistance, and mechanical stability together.
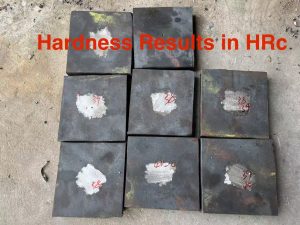
After several days of process optimisation, the final readings across eight samples were:
- 39 HRC
- 38 HRC
- 38–39 HRC
- 38 HRC
- 40–41 HRC
- 39–40 HRC
Every sample met or exceeded the 38 HRC requirement.
7.4 Cutting, machining, and delivery
At that hardness, conventional turning and sawing were no longer practical, so wire cutting was used to hold dimensional accuracy. Final surface grinding followed to bring the finish to specification before dispatch.
After final inspection the material shipped by express, and the customer confirmed satisfaction with both hardness consistency and dimensional accuracy once machining began.
7.5 What the case shows
Two lessons carry over to any hardness-led enquiry:
- Final hardness is a process result, not a composition result. Inconel 901 did not become harder because the chemistry changed; it became harder because the forging and ageing route was controlled deliberately.
- Hardness specifications belong on the enquiry. A target above the standard band changes the raw-material size, the production schedule, and the machining sequence. Naming it late makes the route more expensive than it needs to be.
The same principle runs through the precipitation-hardening grades. Aged Inconel 718 reaches its 36–44 HRC band through a double-ageing cycle, while solid-solution grades hold a stable hardness that cold work and section size move far less. Where a hardness range has to be guaranteed rather than assumed, name it at enquiry so the heat-treatment route can be quoted with the material.
8. Conclusion
The hardness of nickel alloys is not a fixed value but a result of alloy system, processing route, and heat treatment condition.
Hardness conversion tables provide useful engineering references, but they should be used alongside material specifications and heat treatment data.
For high-performance nickel alloys used in demanding environments, understanding the relationship between microstructure and hardness is essential for reliable material selection and process control.
Related reading: our Inconel metal price analysis covers 2026–2027 price trends across Inconel grades. For a primer on the alloy family itself, see our Inconel metal guide.